Alhilal Healthcare
Explore our premium range of clinical-grade personal protection and advanced diagnostic tools, meticulously built to serve global healthcare facilities with uncompromising reliability.
As an industry-leading medical manufacturing enterprise, our factory established in 2009 specialized in the field of disposable personal protective equipment and advanced airway management devices for over 15 years. Today we have more than 500 employees. The company covers an area of more than 100,000 square meters and has a clean workshop of 6,000 square meters.
The factory mainly produces and sells non woven medical face masks, disposable coverall, surgical gowns, disposable shoes cover, disposable medical boot covers, disposable bed sheet, disposable caps, disposable lab coats, lab jackets, isolation gowns, scrub suits, aprons, sleeves cover, etc. For the better promising quality to our customers, our company has passed the factory audit report from ISO13485, CE. All our products meet the high levels of quality demand and conform to worldwide regulatory benchmarks.
Our state-of-the-art facilities leverage cutting-edge automation technology, stringent raw material selection, and rigorous multi-stage laboratory testing to ensure zero-defect production for critical care products including endotracheal tubes and surgical supplies.
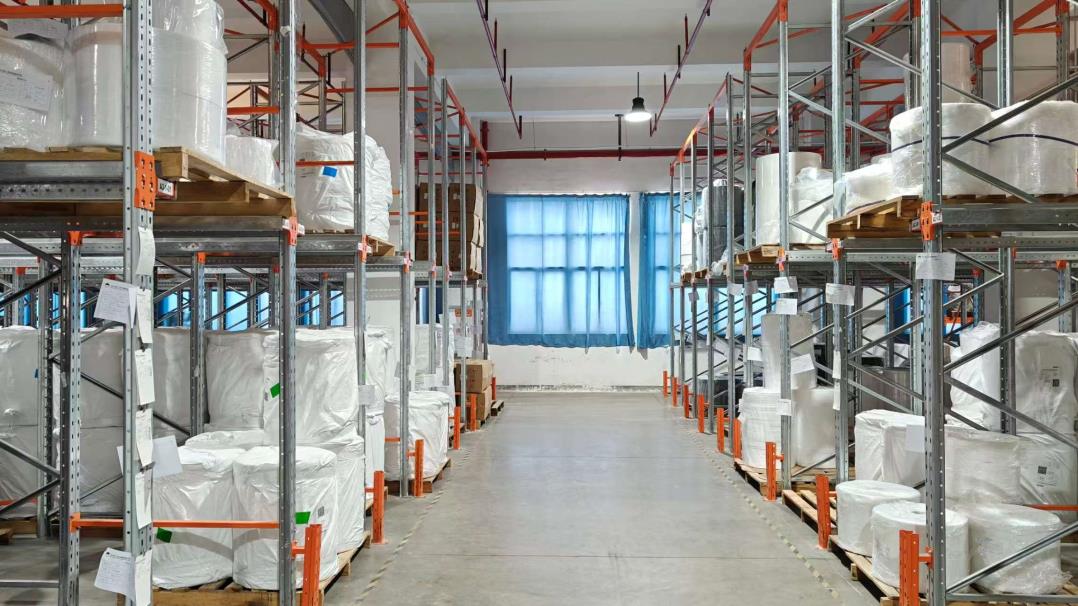
Sourcing biocompatible, medical-grade raw polymers to guarantee patient safety and ultimate airway comfort.
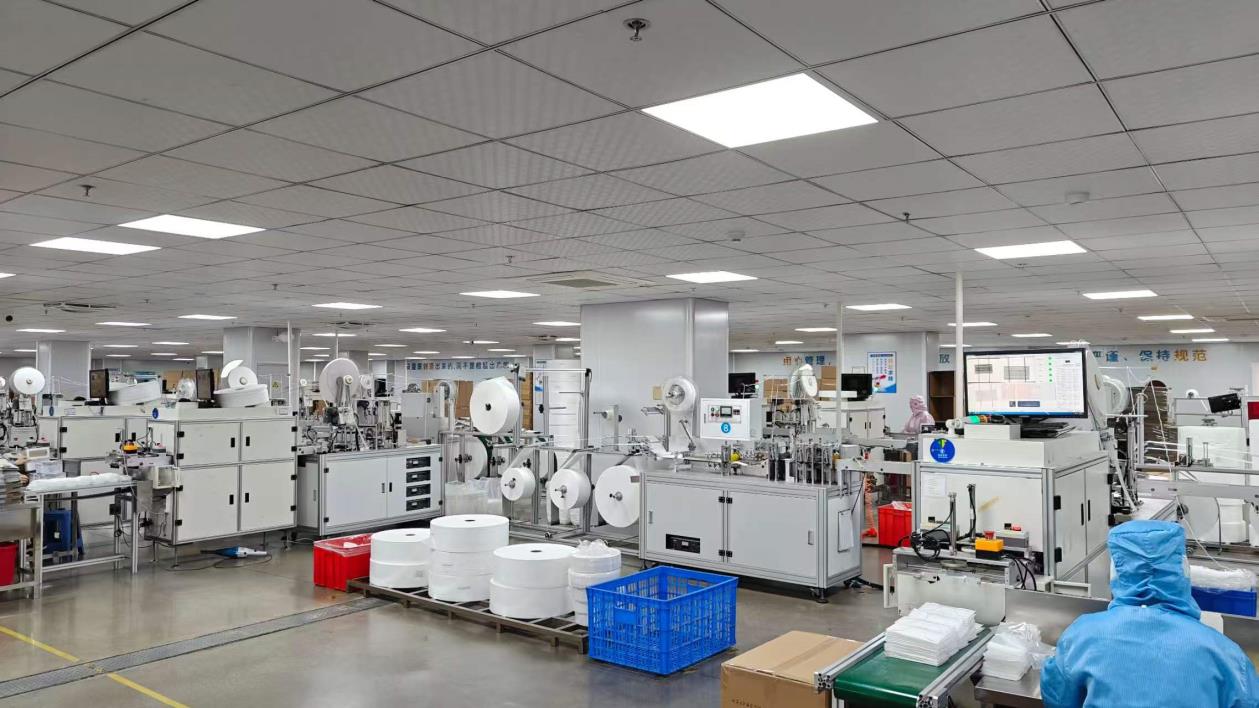
High-precision automated manufacturing lines ensuring consistent dimensions and structural integrity.
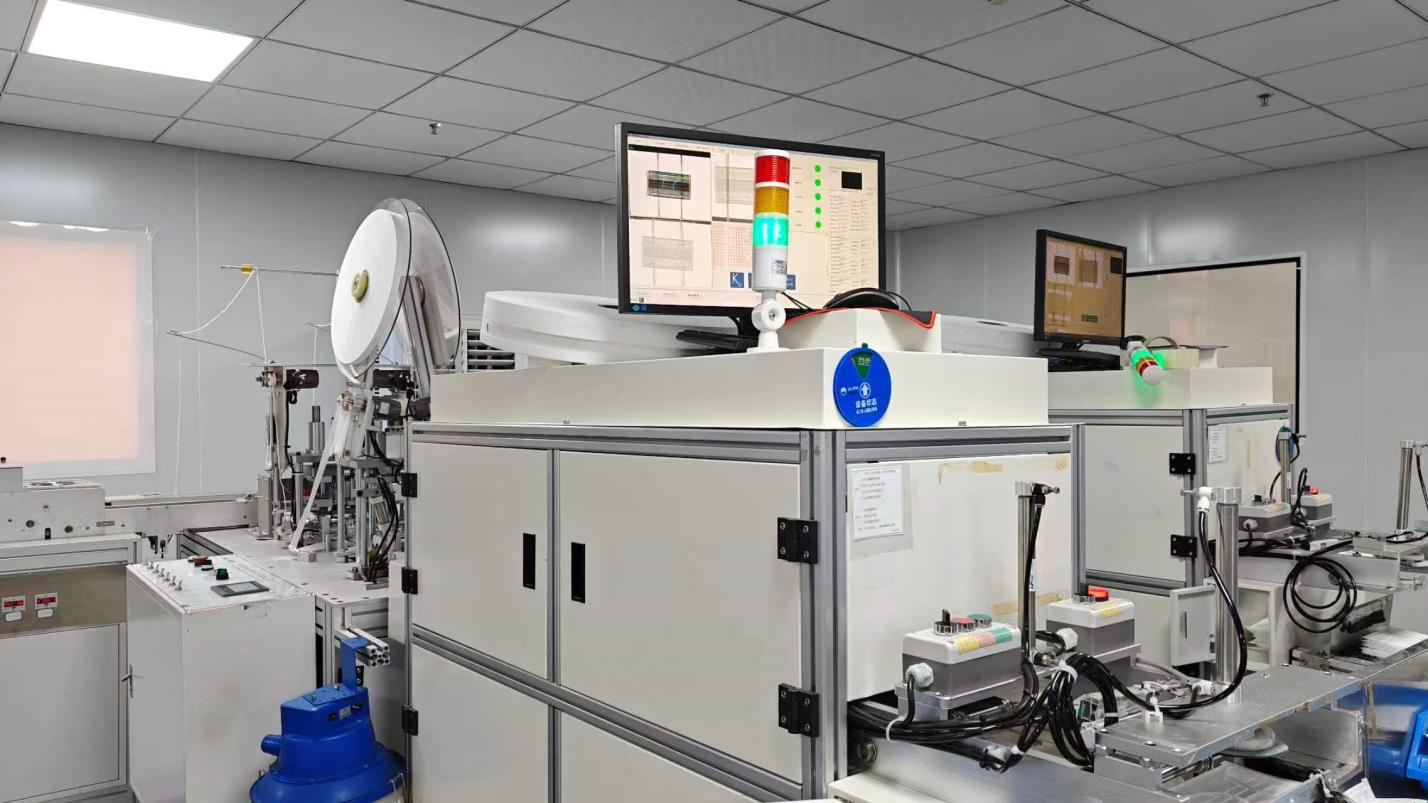
Vision-based scanning systems to eliminate microscopic flaws prior to final assembly and sterilization.
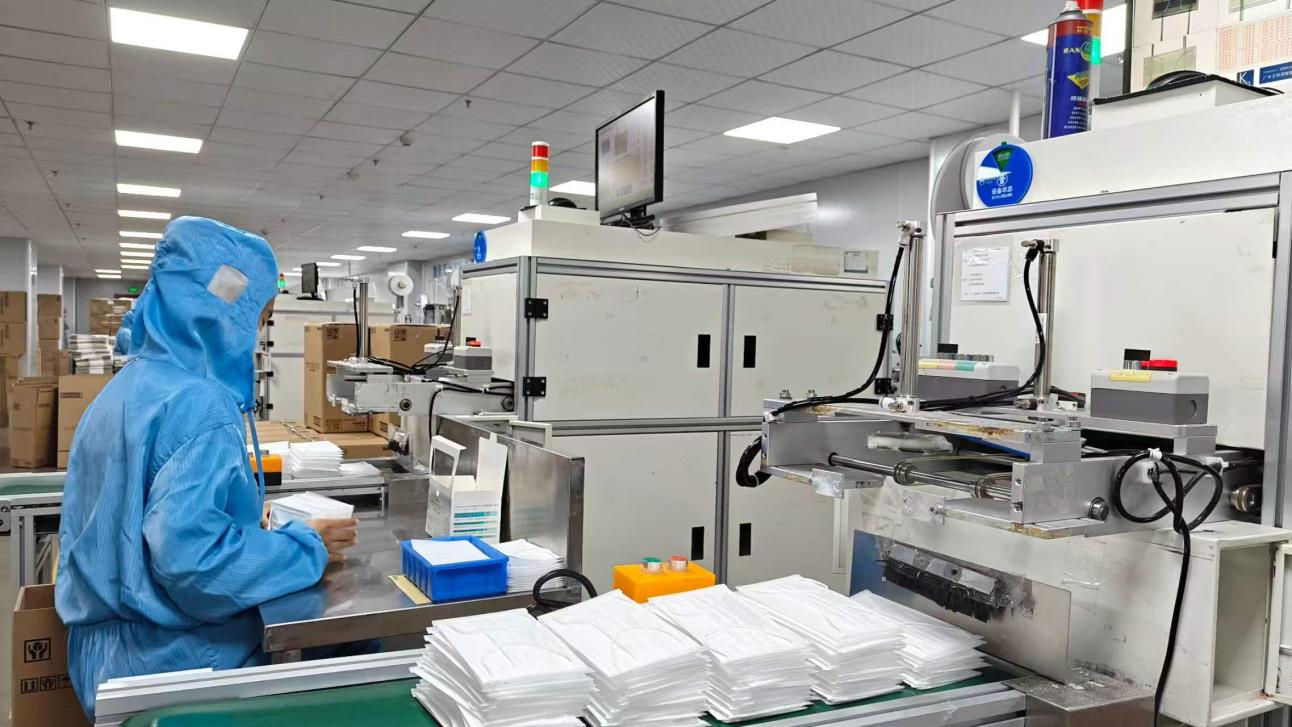
Cleanroom packaging environments maintaining sterile conditions for international delivery.
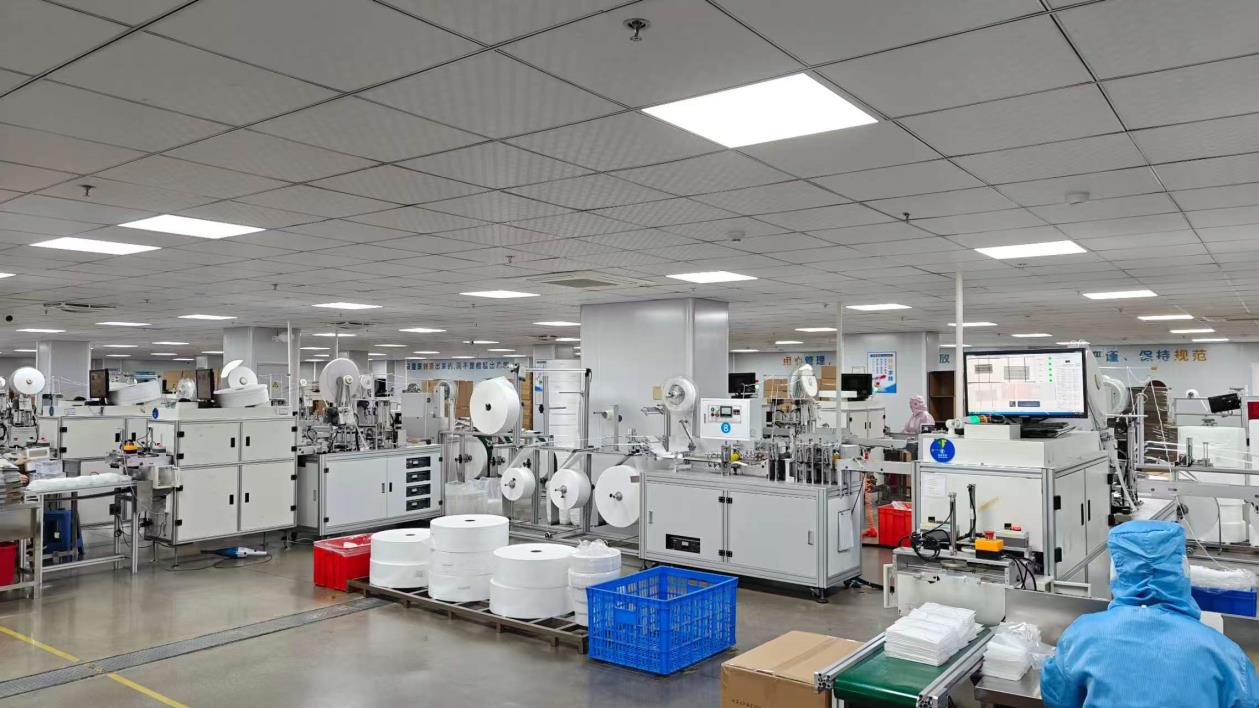
High-speed ultrasonic welding lines for superior filtration efficiency and breathability.
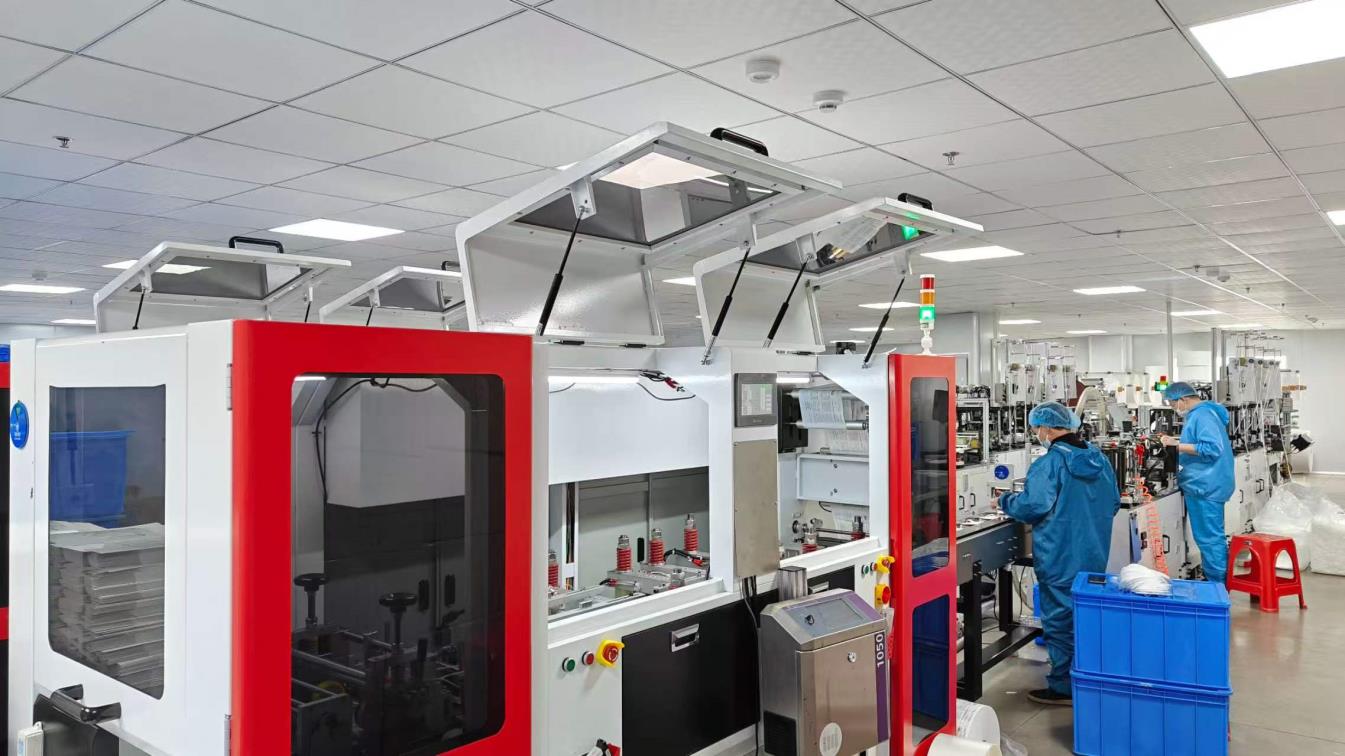
Advanced shaping technology delivering robust multi-layer protection standards.
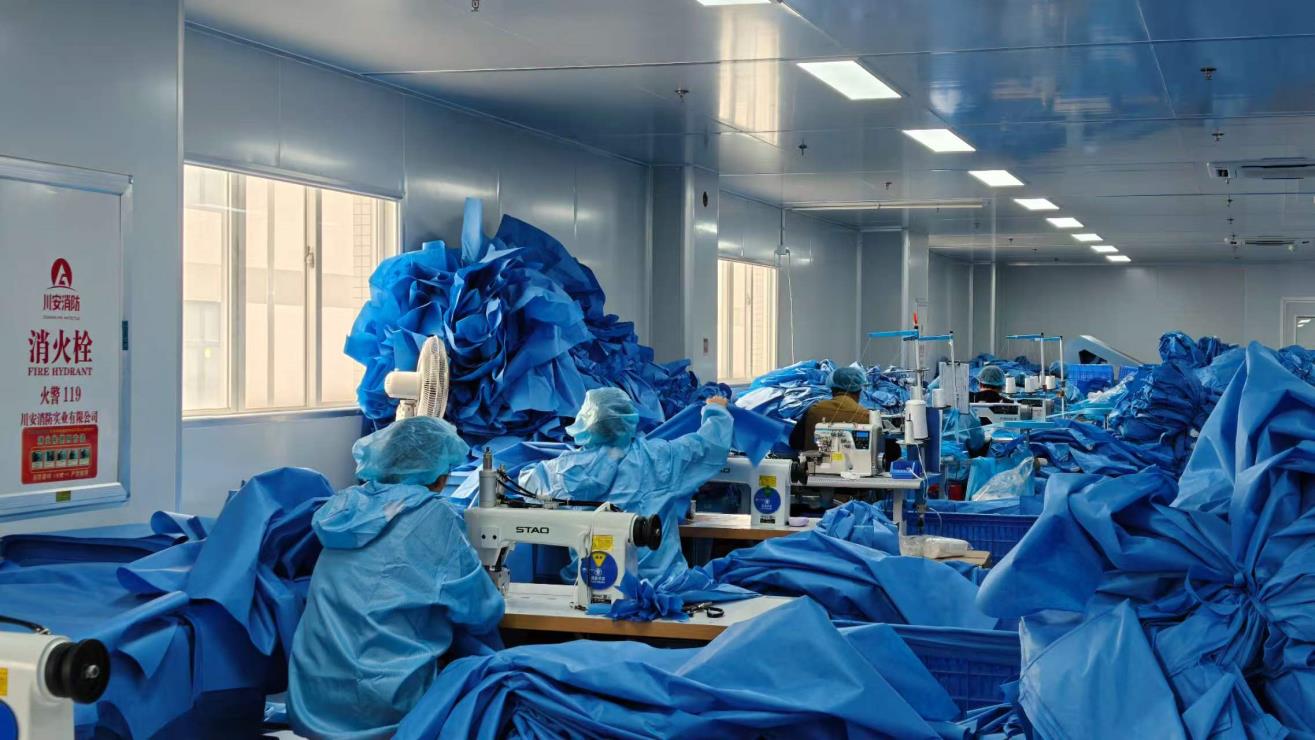
Ergonomically designed garment manufacturing units operated by seasoned professionals.
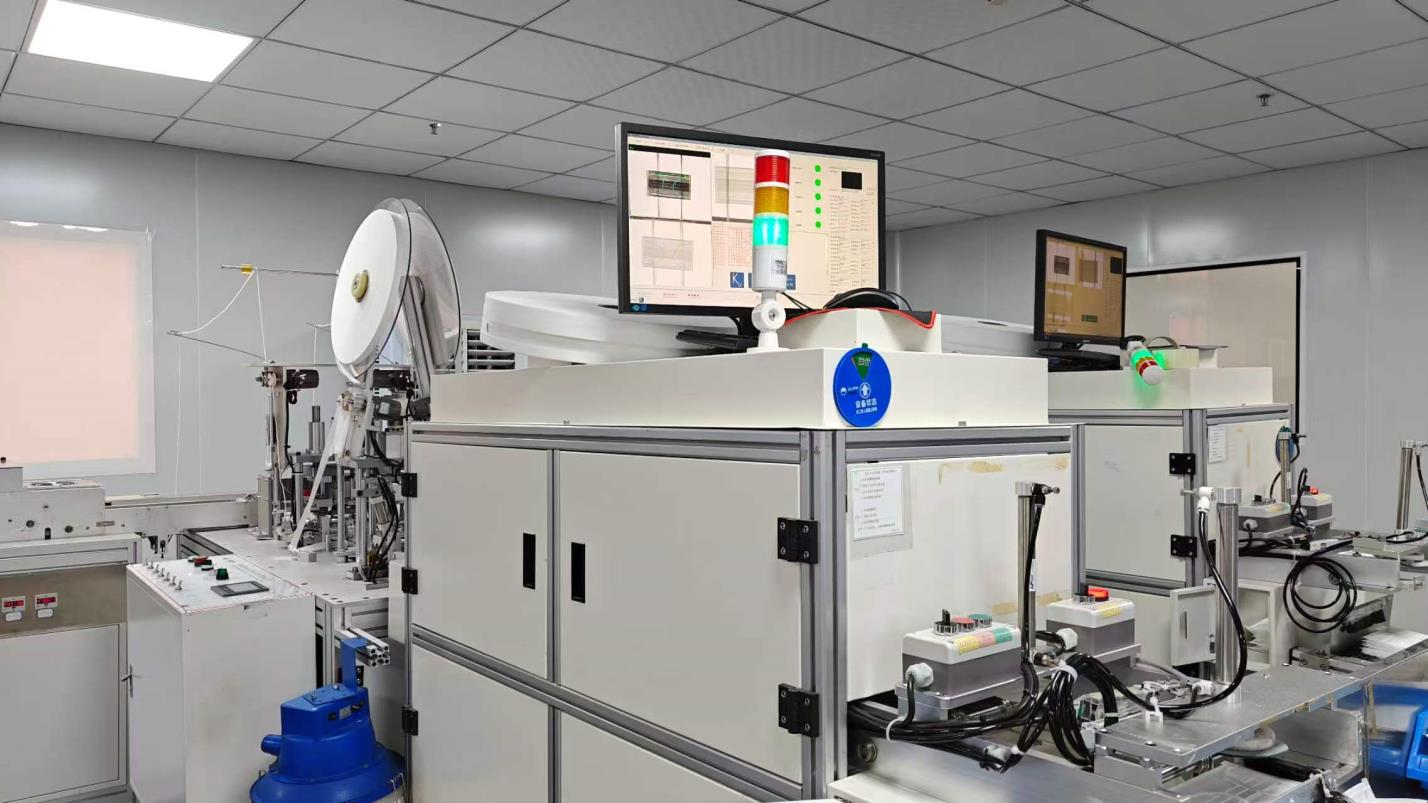
Continuous inline parameter checking for real-time quality assurance optimization.
To meet the exacting demands of global procurement teams, our in-house testing laboratory conducts comprehensive physical, chemical, and microbiological evaluations on every production batch.
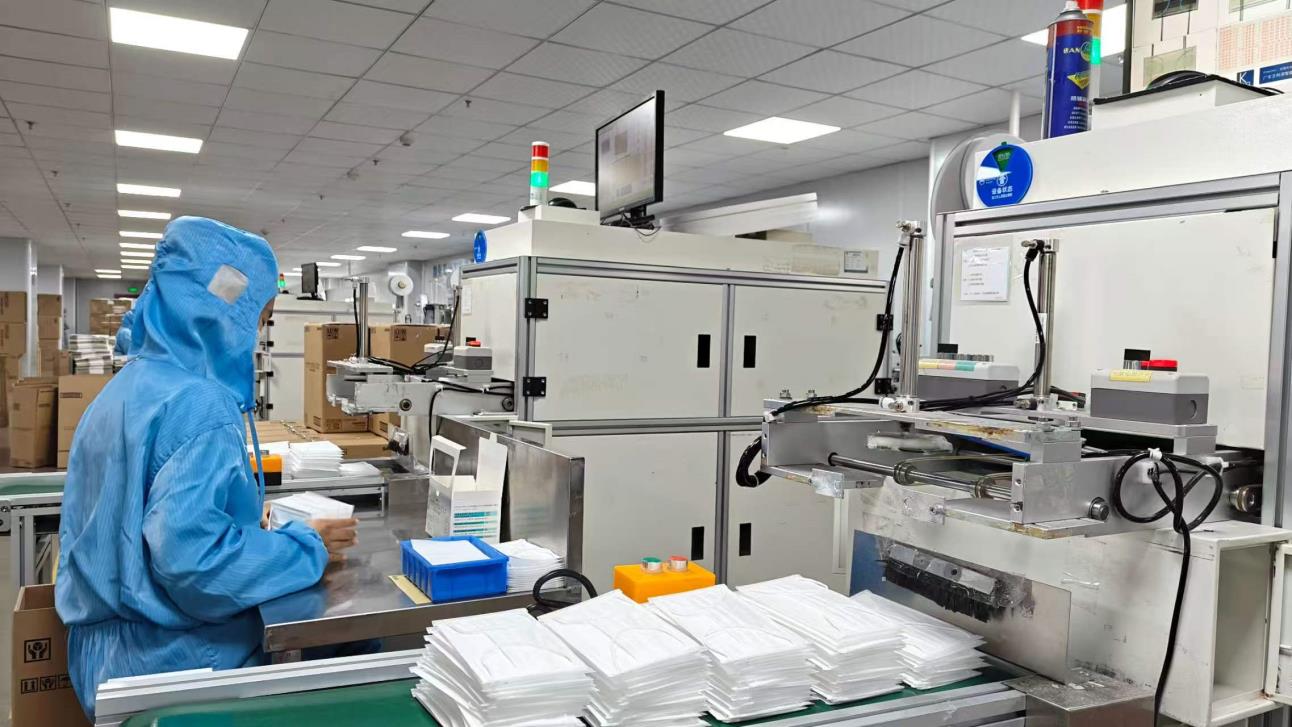
Comprehensive physical durability and tensile strength testing for all medical polymers.
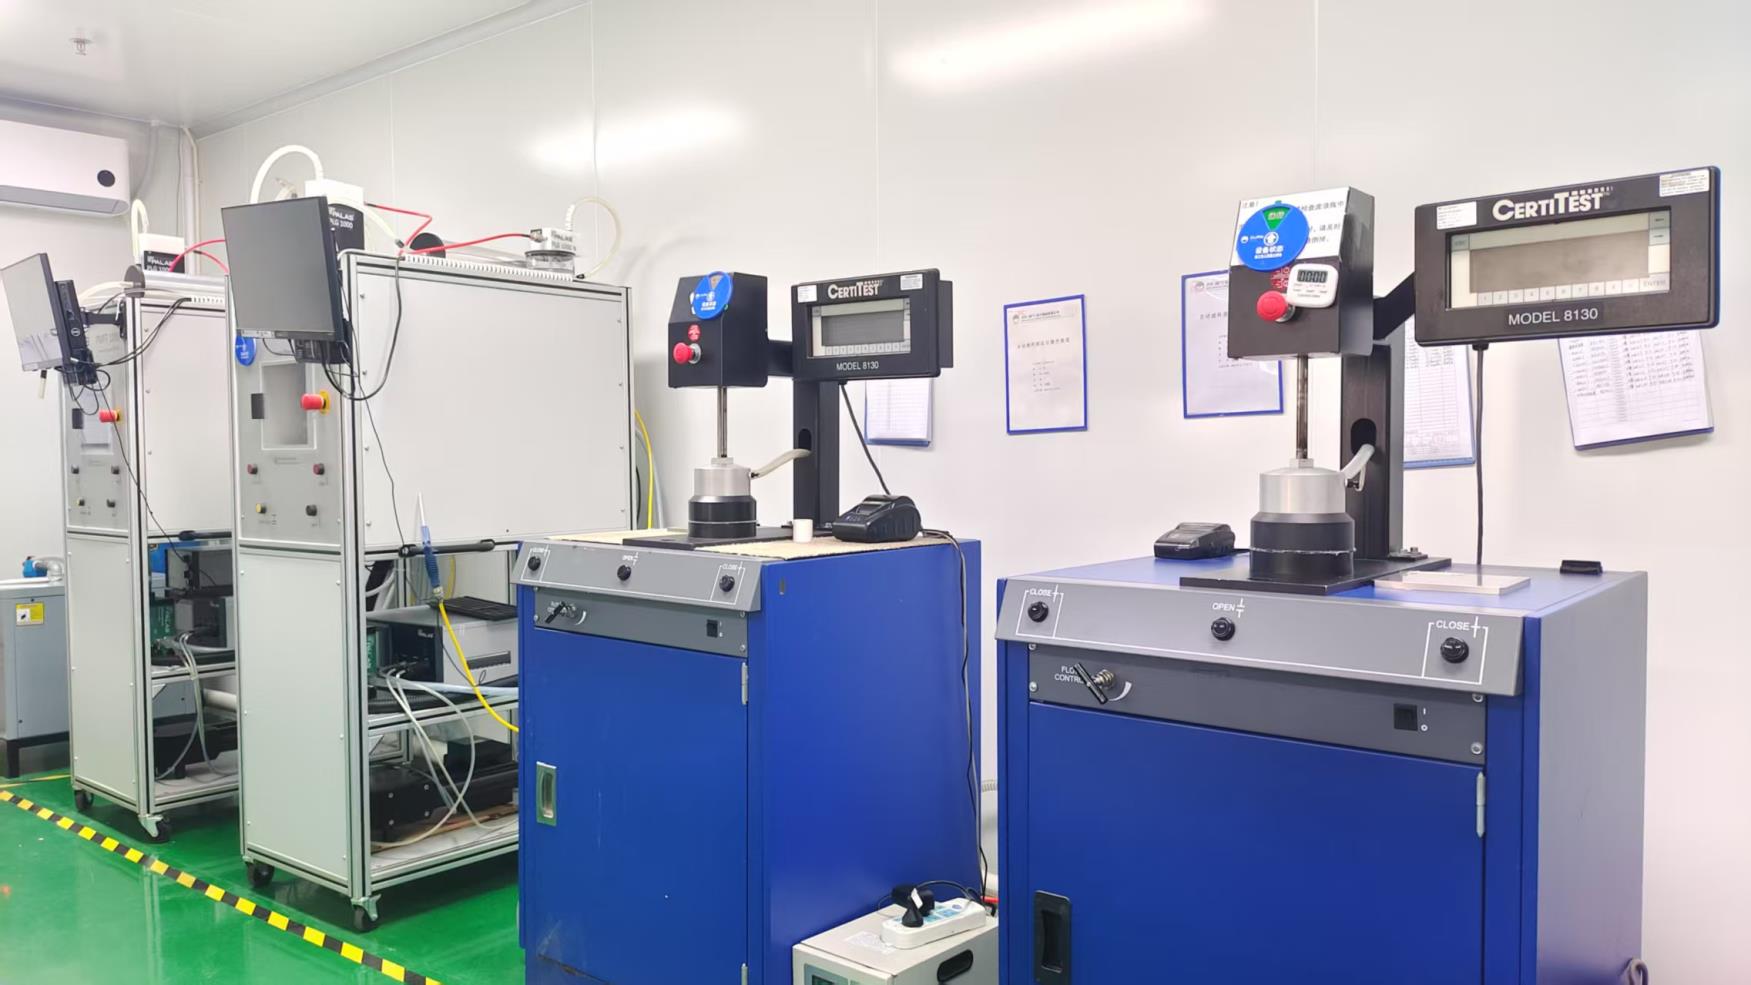
Evaluating particulate filtration efficiency (BFE/PFE) under simulated clinical respiration conditions.
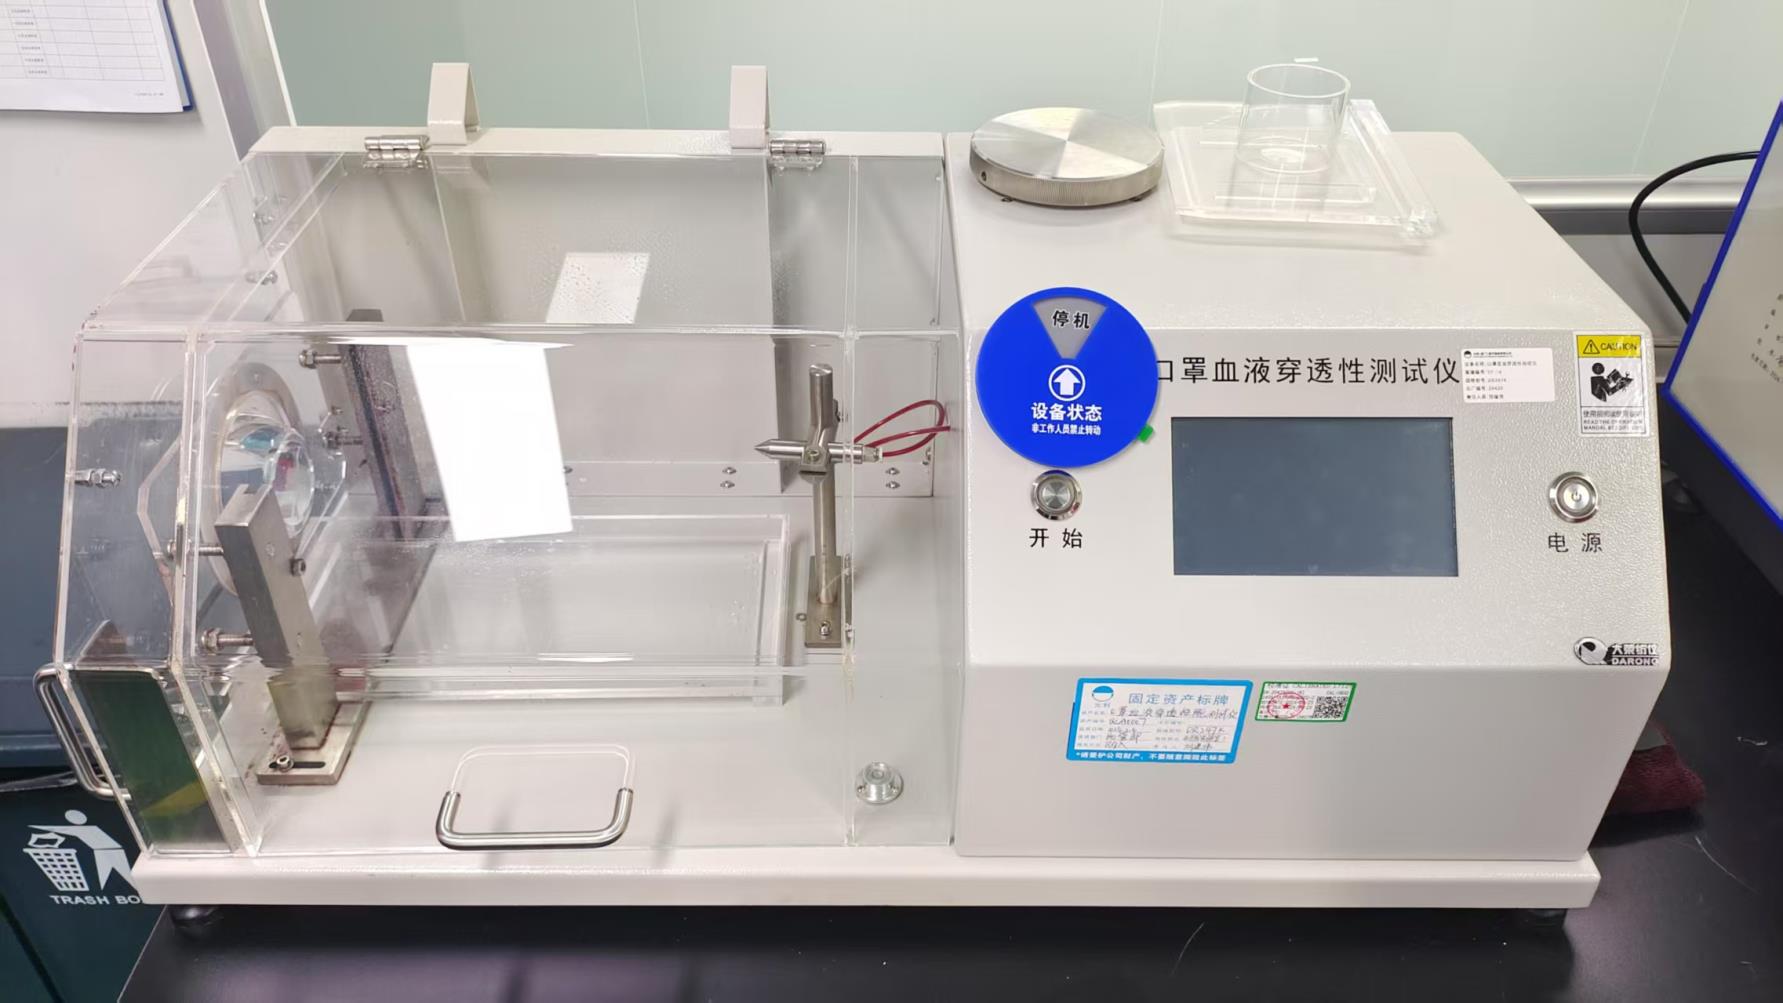
Ensuring absolute fluid barrier protection against bloodborne pathogens and infectious liquids.
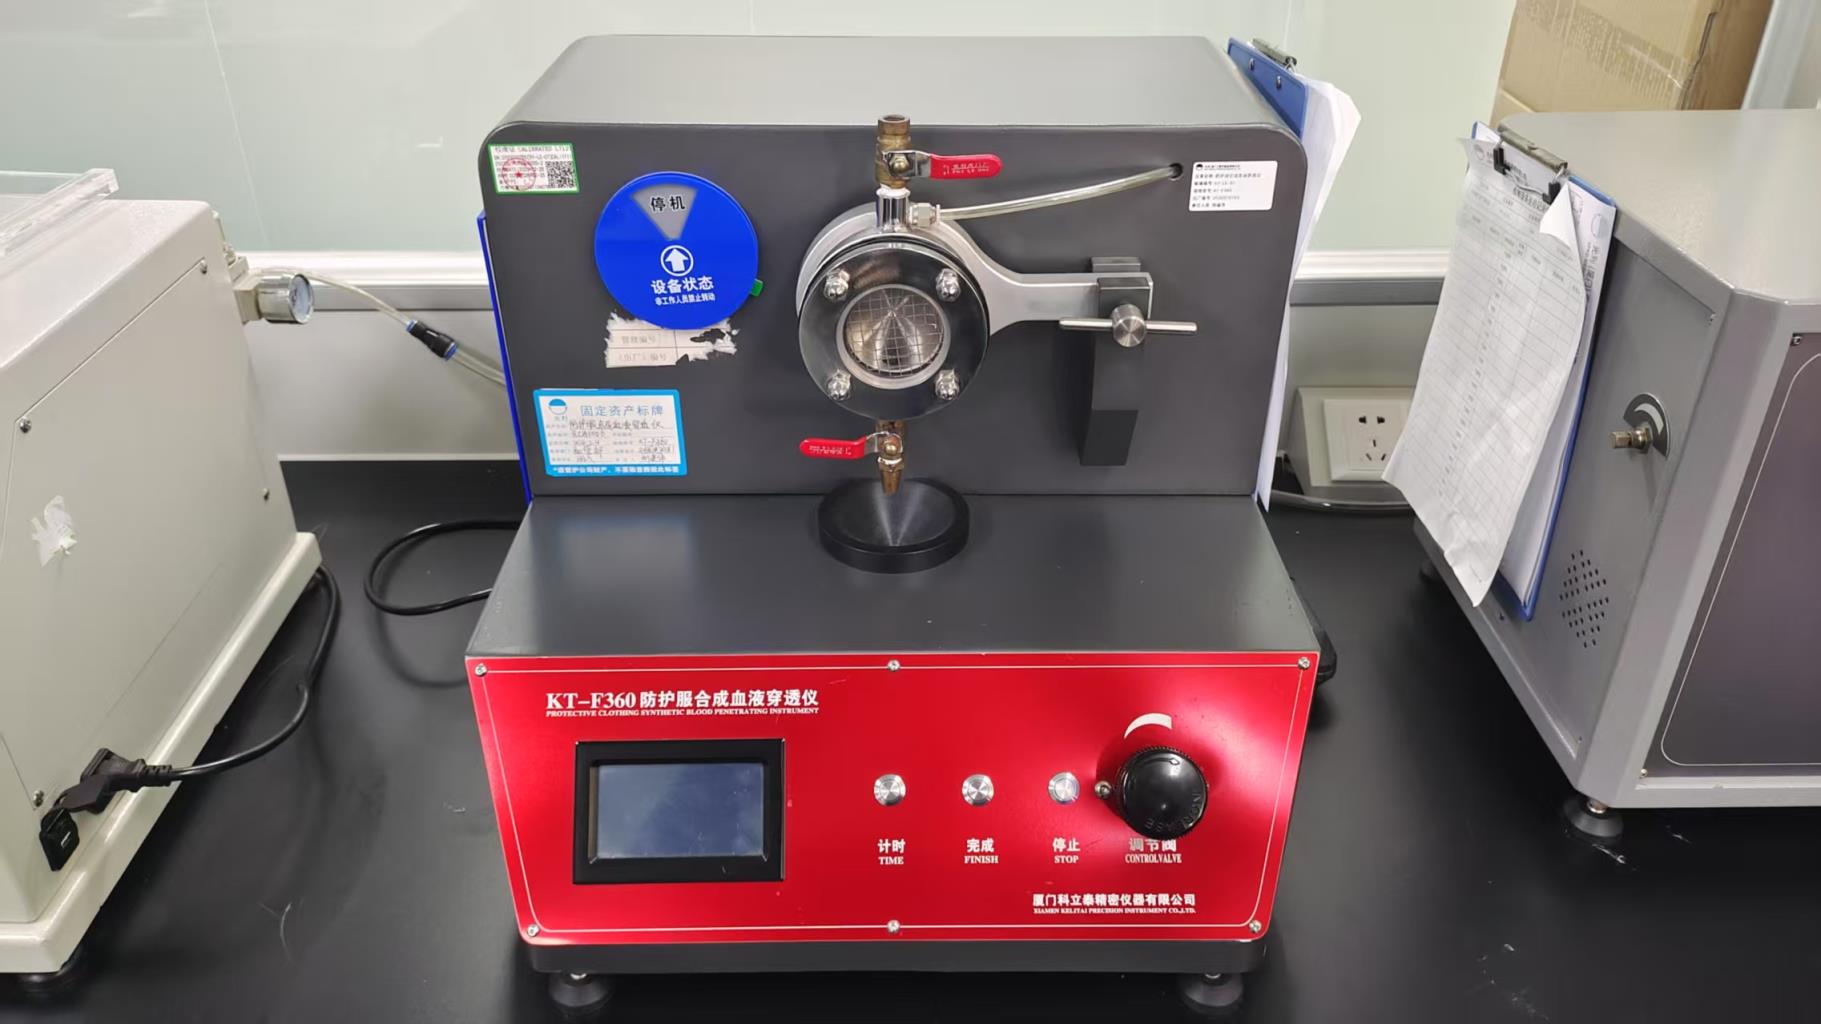
High-pressure resistance verification for protective clothing and surgical barriers.
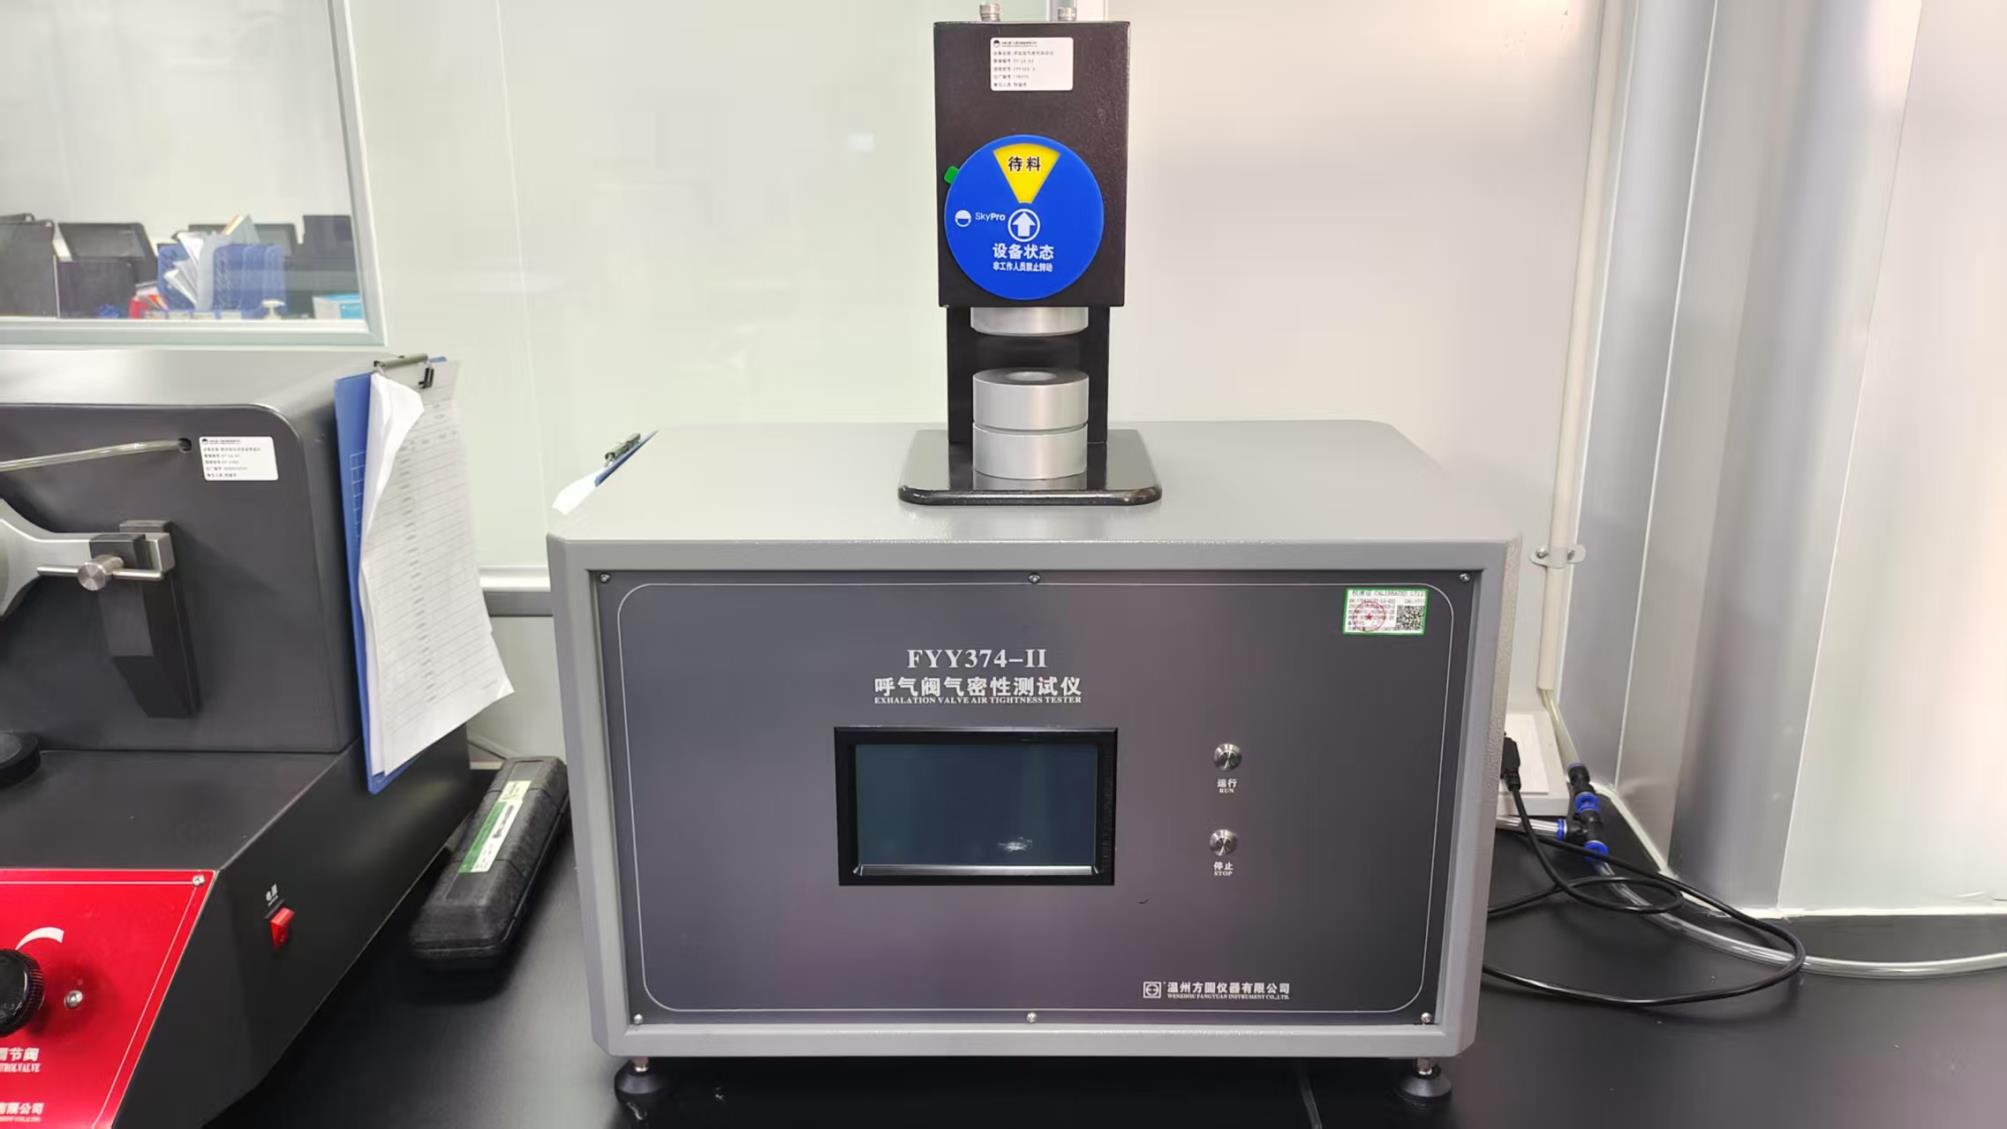
Verifying valve sealing precision to prevent unfiltered air leakage in respiratory units.
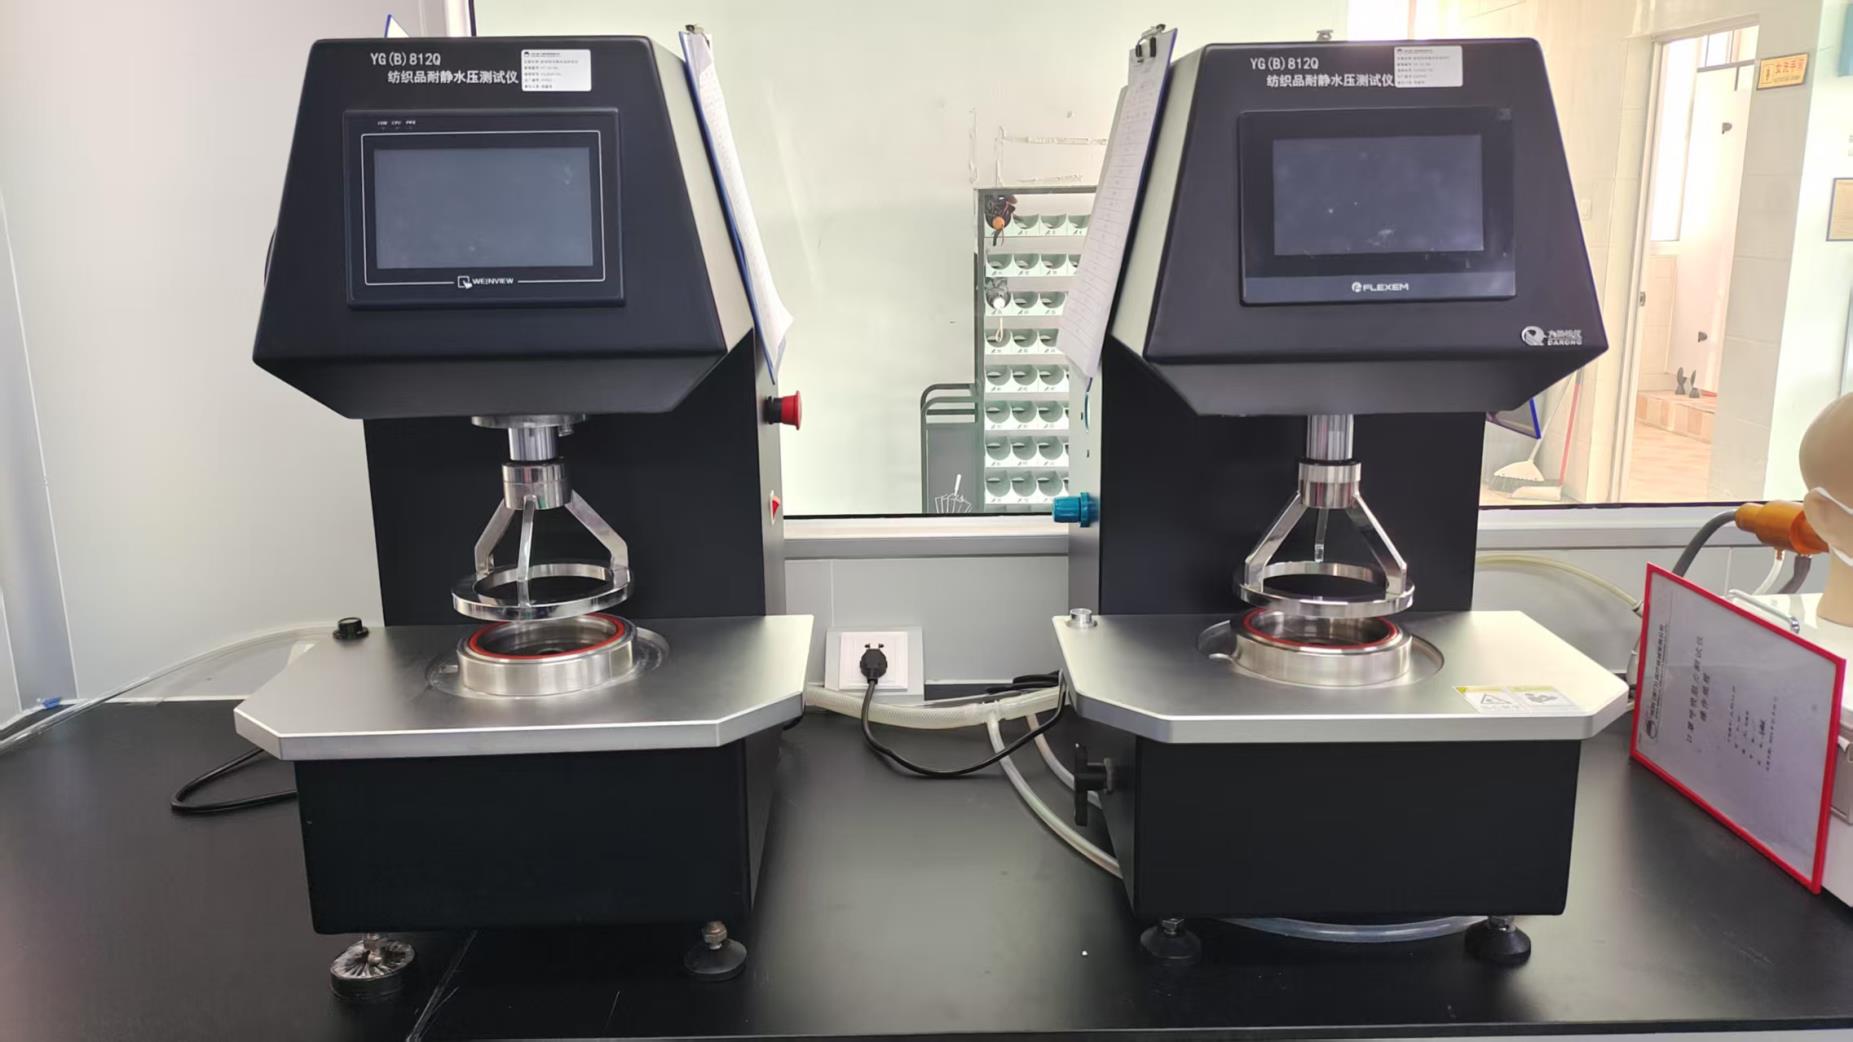
Assessing water resistance thresholds for medical textiles and non-woven isolation fabrics.
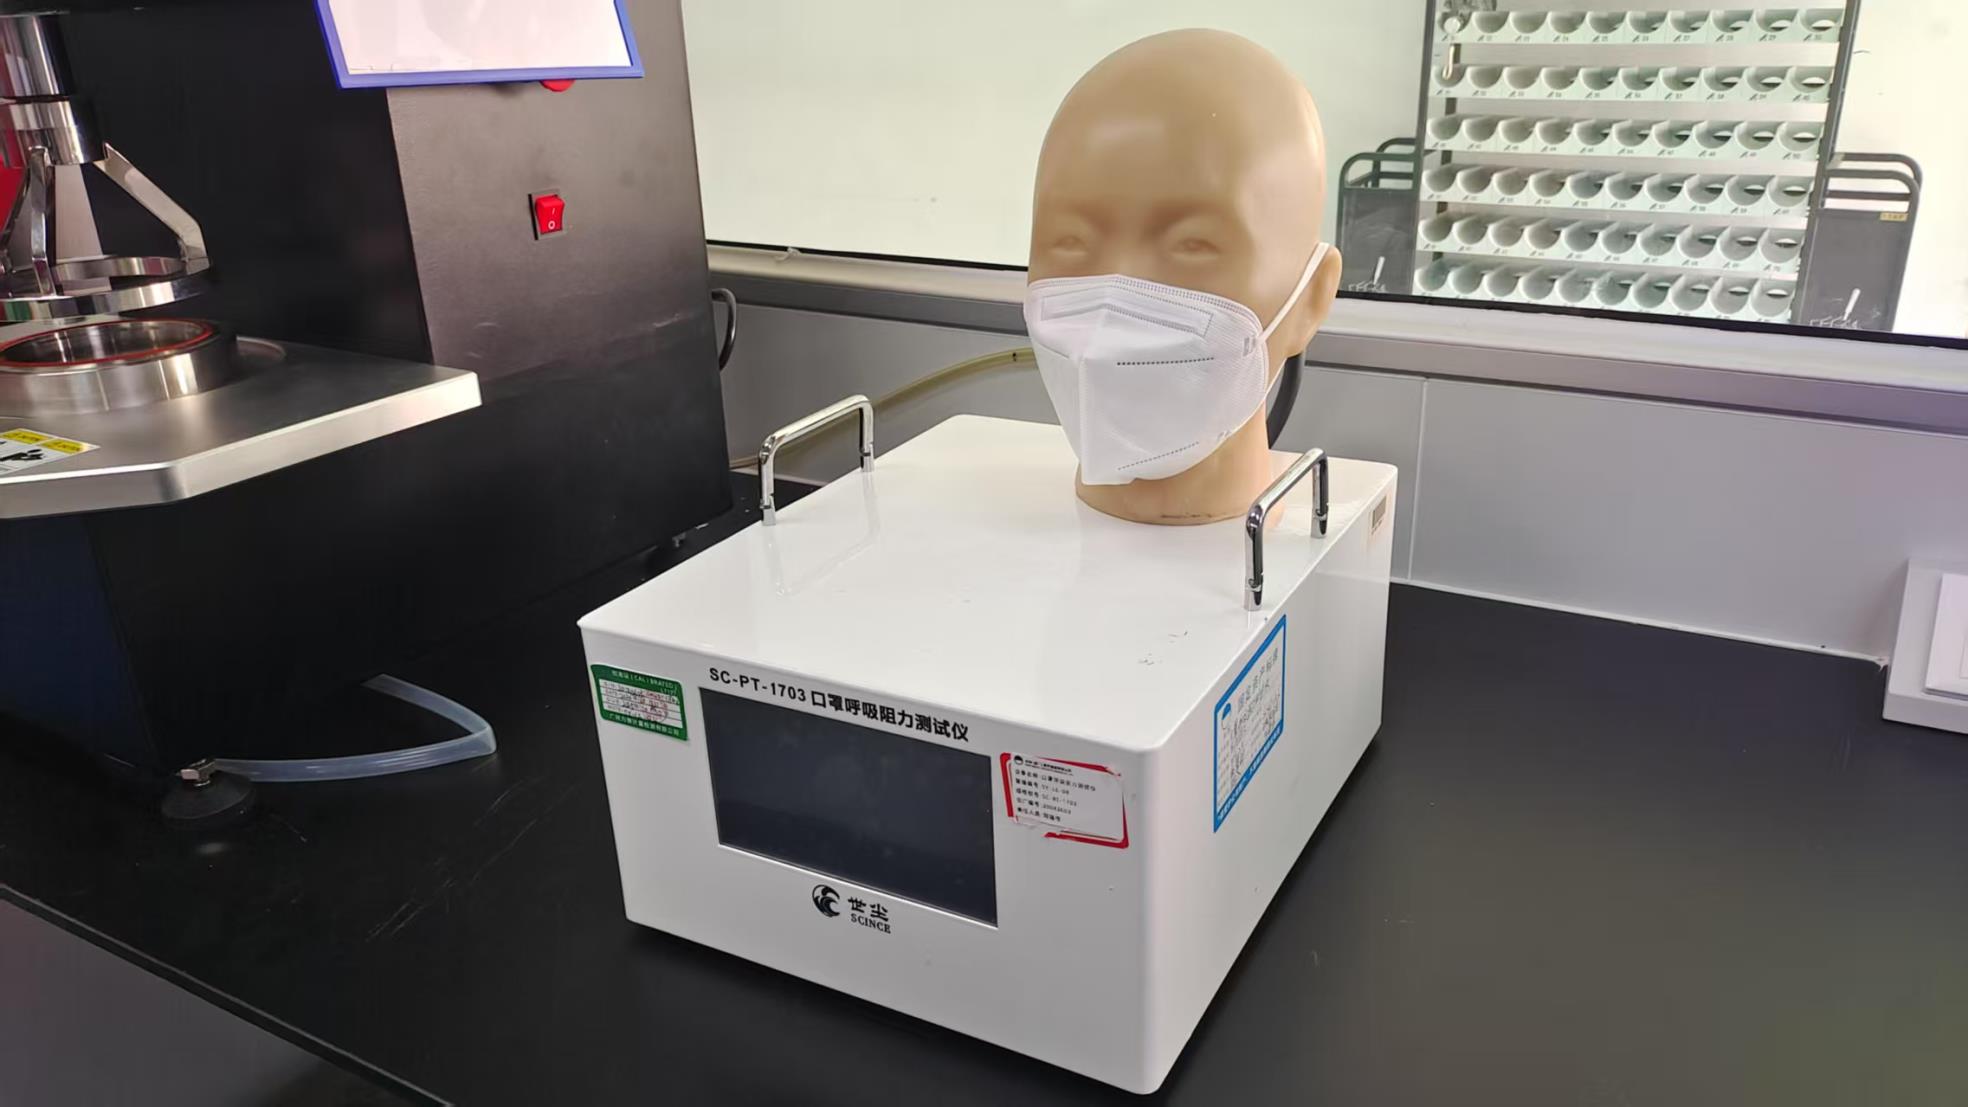
Measuring inhalation and exhalation pressure drops for optimal user comfort and safety.
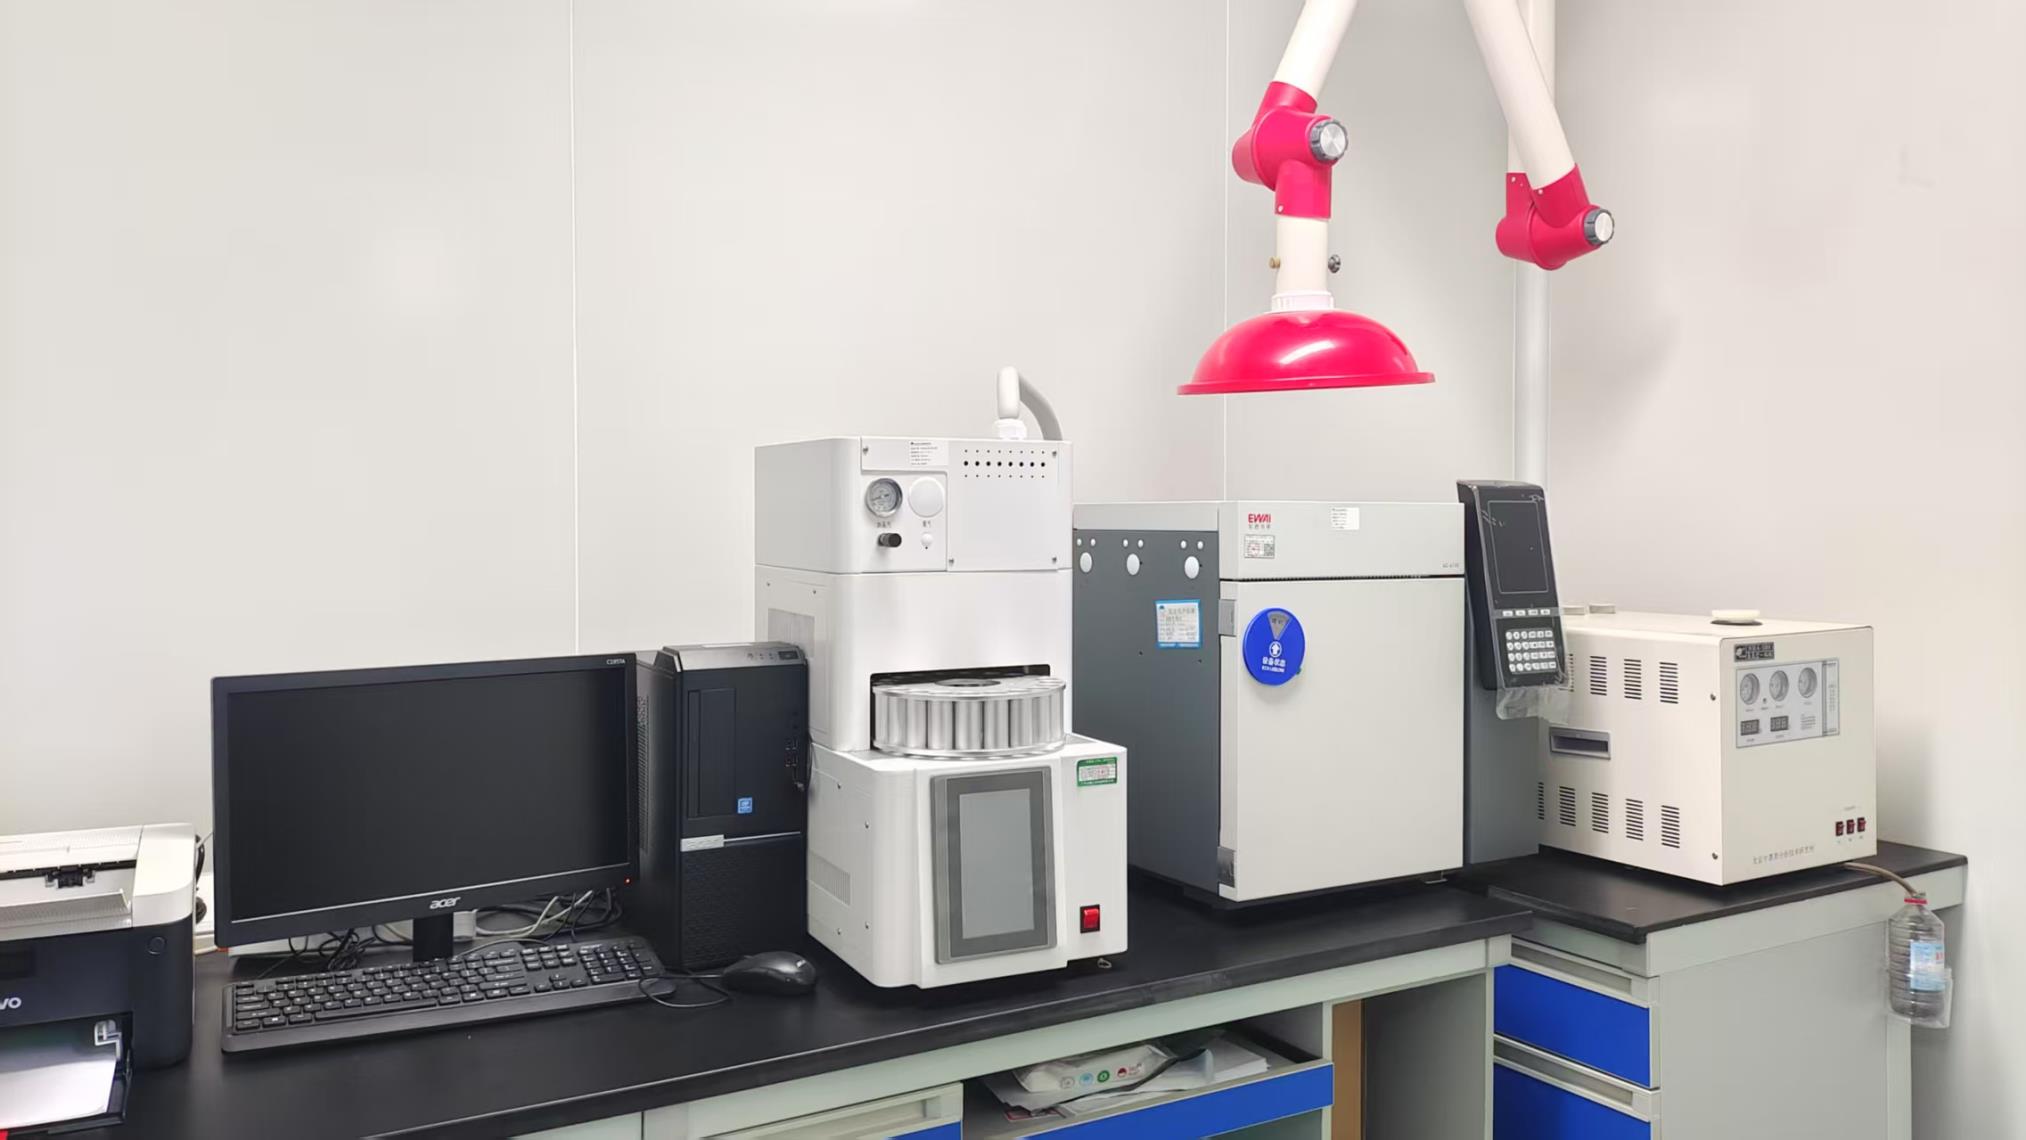
Detecting and quantifying residual ethylene oxide or organic volatiles post-sterilization.
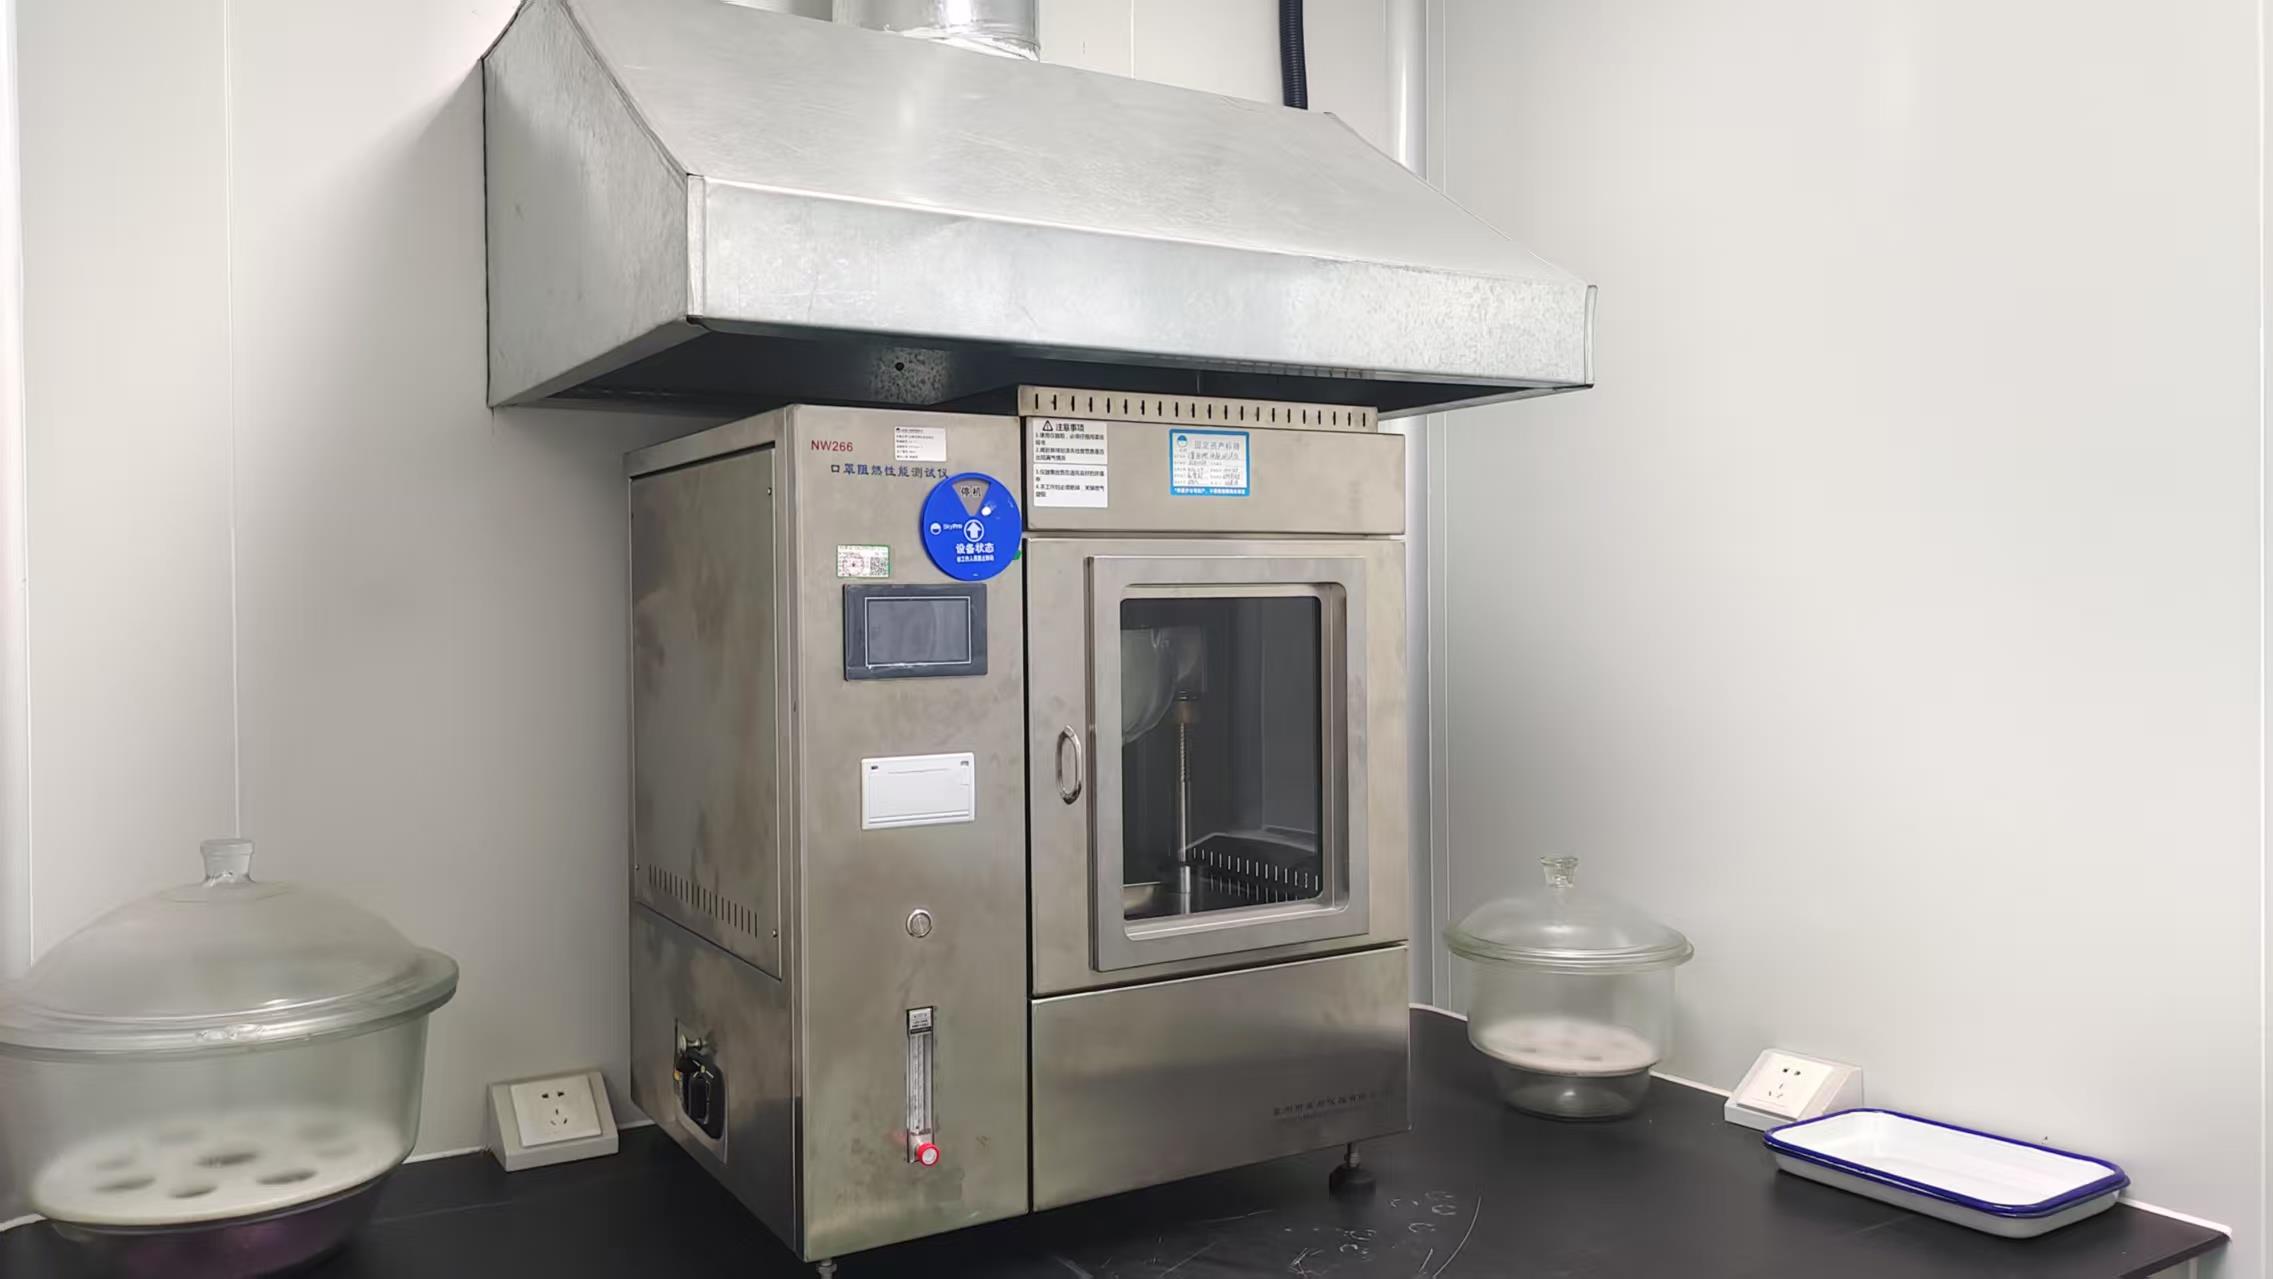
Ensuring materials meet strict anti-flammability standards for operating room environments.
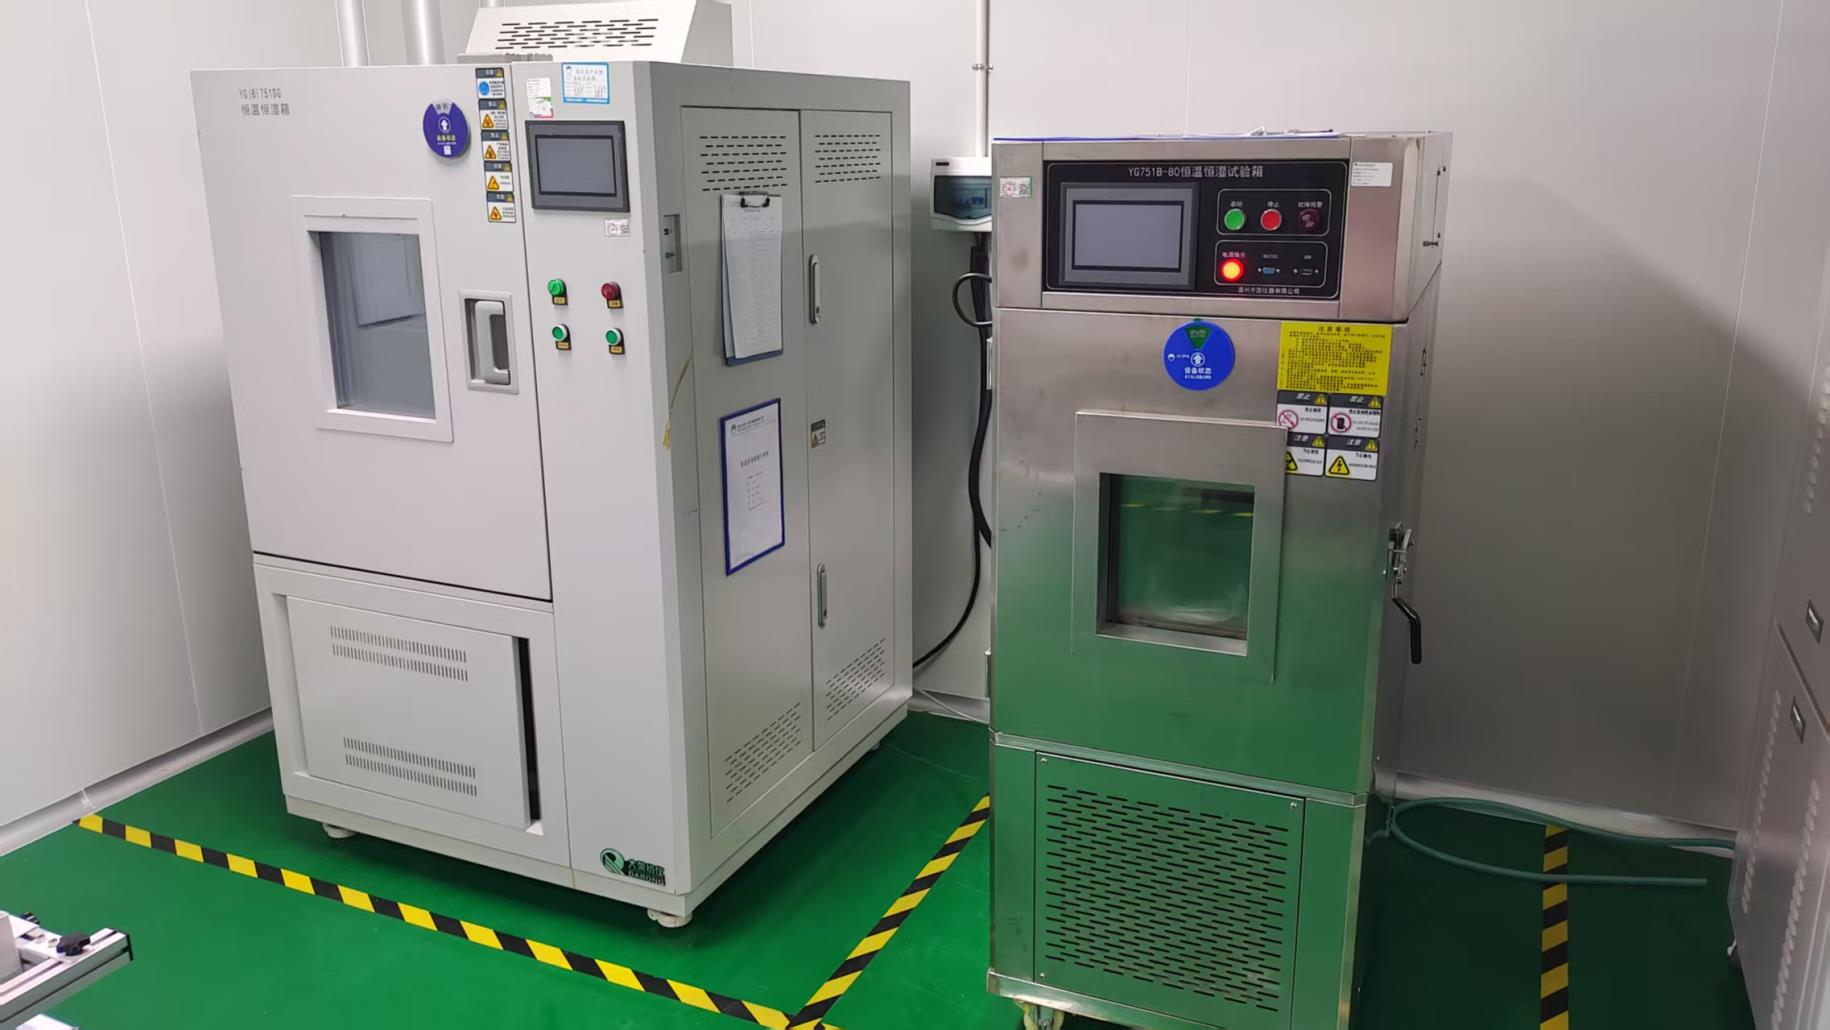
Simulating extreme environmental storage conditions to test packaging and product shelf-life.
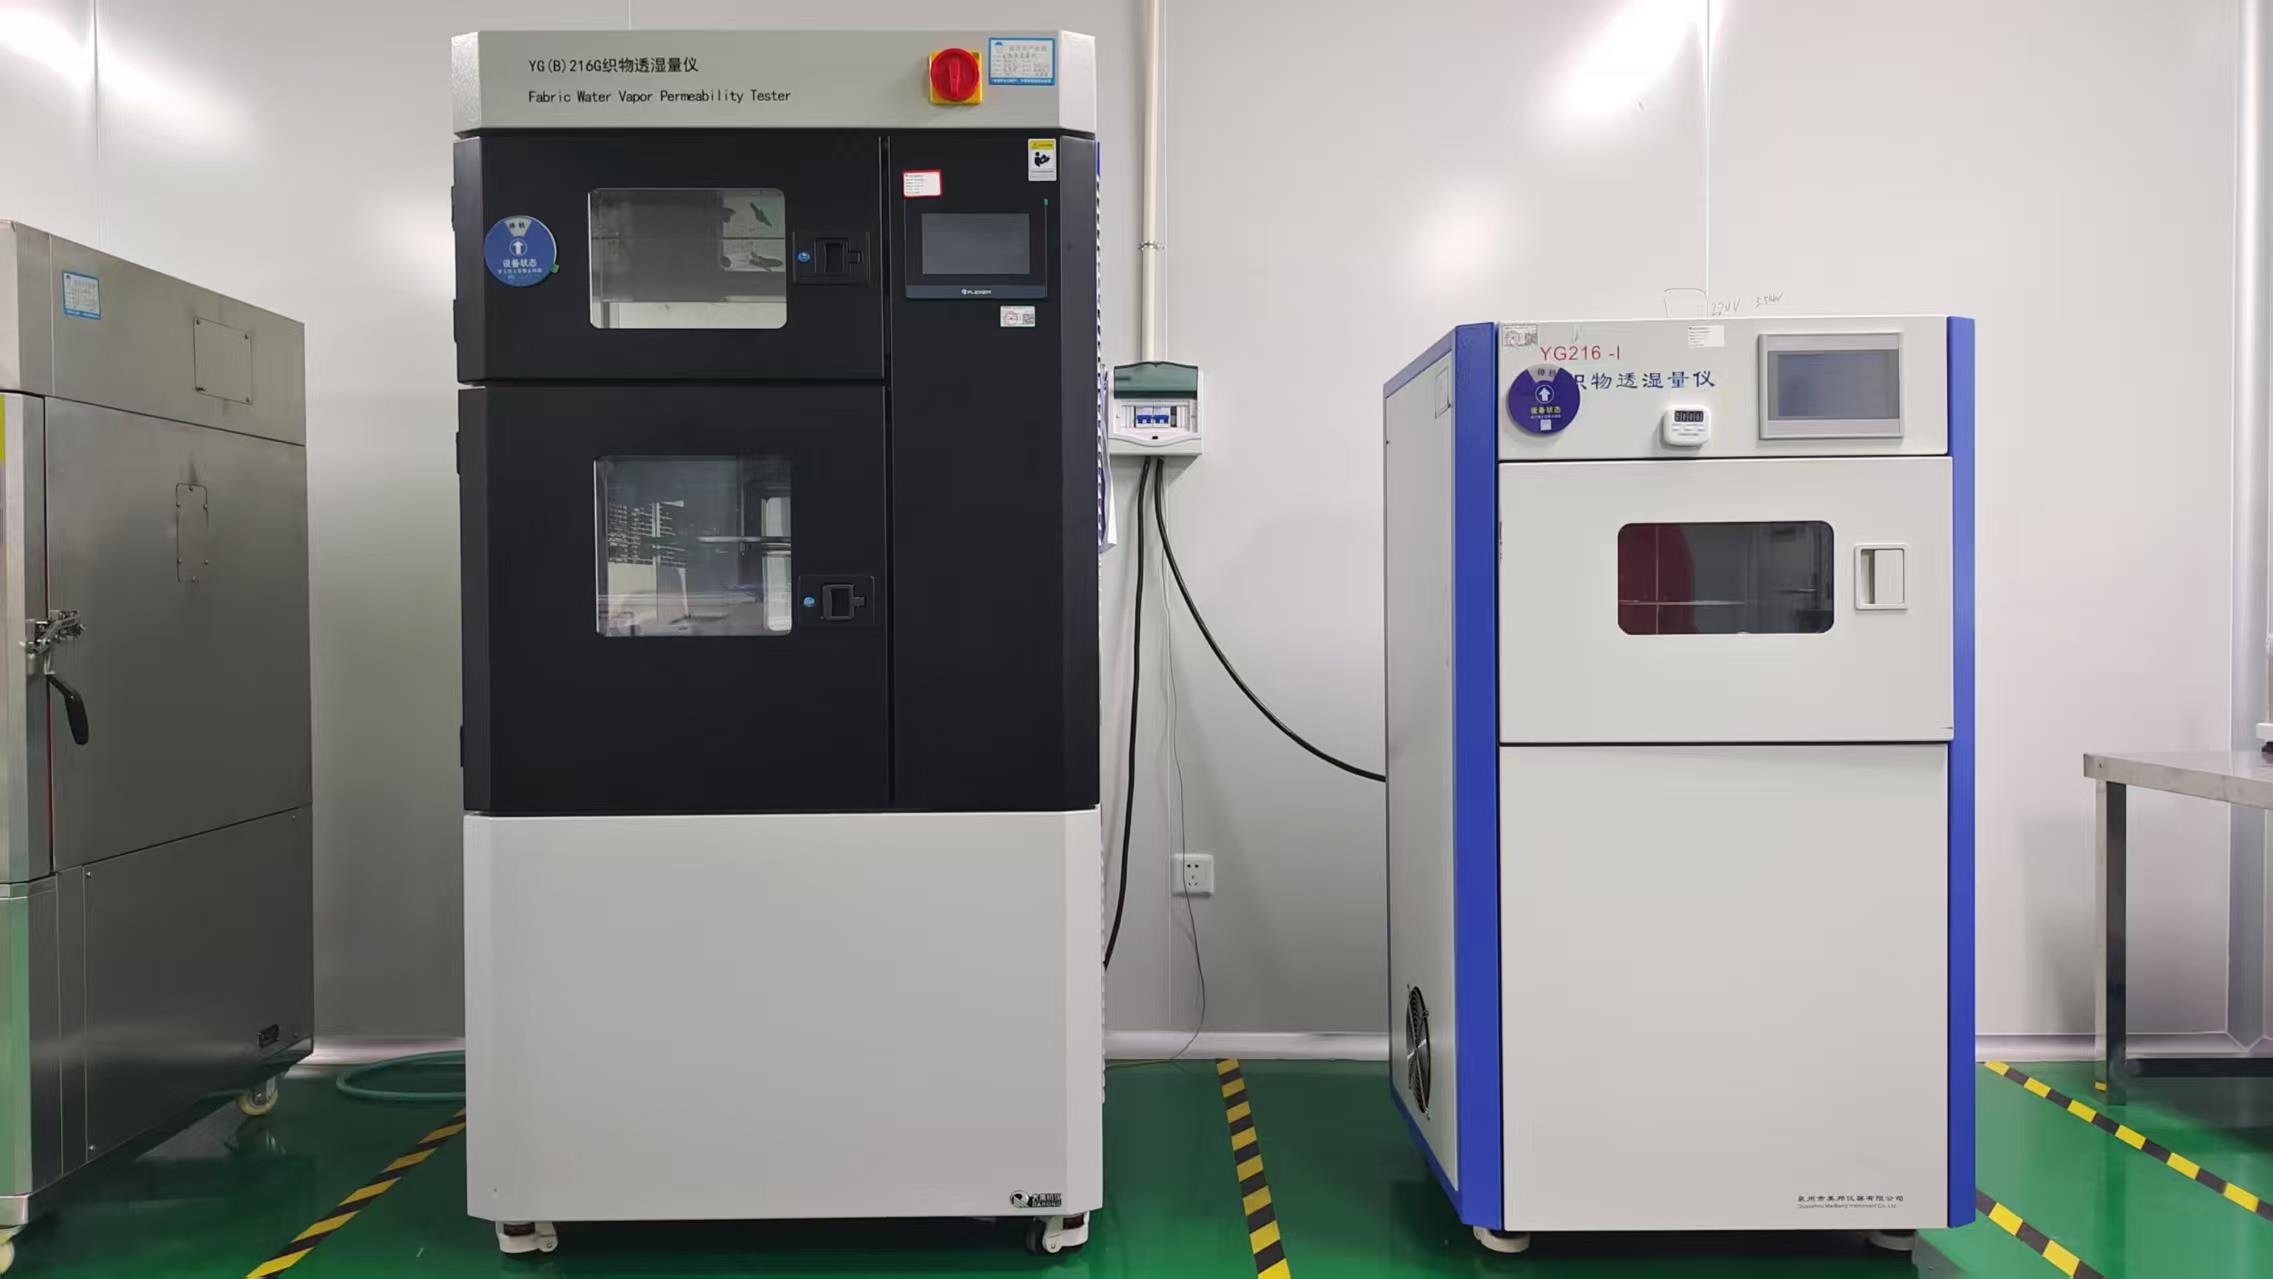
Measuring moisture management capabilities to prevent heat stress during prolonged surgical procedures.
Modern hospital groups, government health agencies, and medical distributors face unprecedented demands for supply chain resilience, transparent quality auditing, and cost-effective volume scaling. As a premier manufacturer of critical airway management tools and protective medical consumables, we bridge the gap between advanced clinical requirements and large-scale manufacturing efficiency.
Our localized support teams and streamlined logistics network ensure uninterrupted fulfillment across North America, Europe, Southeast Asia, and the Middle East, complying fully with regional medical device regulations.
The medical device landscape is rapidly evolving towards enhanced patient comfort, reduced trauma during intubation, and smart infection control. Innovations in soft medical polymers, high-volume low-pressure cuffs, and radio-opaque lines are setting new benchmarks for endotracheal tube safety.
By integrating cutting-edge automated production with rigorous ISO13485 quality management systems, our factory remains at the forefront of delivering dependable, life-saving equipment to healthcare professionals worldwide.
Our manufacturing facility and product lines are fully certified under ISO13485 quality management standards and carry CE marks, confirming compliance with international medical device directives for safety, efficacy, and quality assurance.
Yes, we specialize in OEM and ODM partnerships. With our 100,000+ square meter manufacturing base, advanced automated machinery, and dedicated R&D engineering team, we can customize product dimensions, packaging configurations, and branding to meet your exact institutional requirements.
We utilize cleanroom production environments coupled with automated optical detection systems and comprehensive in-house laboratory testing (including gas chromatography, burst pressure testing, and microbial barrier evaluation) to guarantee 100% batch consistency and absolute sterility.
Thanks to our large-scale automated production lines and robust raw material inventory, standard bulk orders are typically fulfilled and dispatched within 15 to 30 days, depending on order volume and custom packaging specifications.
Browse further through our extensive catalogue of specialized endoscopic equipment, monitoring systems, and disposable hospital supplies.

Medical Veterinary Surgery Equipment Surgical Laparoscopic Instruments Ultrasonic Scalpel System
View Product
Digital Wireless Stress ECG Systems (only Software) , Monitoring of Running Heart State
View Product
Portable Endoscopy Camera Telepack Endoscope Camera System for Ent/Laparoscopy/Hysteroscopy/Urology
View Product