Alhilal Healthcare
Explore our flagship certified medical supplies, high-efficiency barrier gowns, precision endoscopic systems, and protective cleanroom apparel manufactured under rigorous ISO 13485 oversight.

Established in 2009, our modern industrial complex has spent over 15 years engineering world-class personal protective equipment, custom surgical instrument trays, and sterile processing solutions for top-tier healthcare systems worldwide.
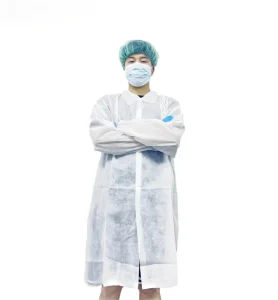
Our integrated manufacturing plants are equipped for high-capacity output across diverse sterile non-woven, polymeric, and mechanical product categories. Our primary portfolio includes: non-woven medical face masks, disposable coveralls, surgical gowns, disposable shoe covers, disposable medical boot covers, disposable bed sheets, surgical caps, lab coats, lab jackets, isolation gowns, scrub suits, protective aprons, sleeve covers, and customized OEM/ODM surgical instrument trays.
A comprehensive analysis of design methodologies, material science, sterile processing compatibility, and supply chain strategies in modern surgical asset management.
The contemporary Operating Room (OR) and Central Sterile Supply Department (CSSD) demand stringent hygiene standards, ultra-durable containment systems, and rapid turnaround cycles. Surgical instrument trays—ranging from stainless steel mesh baskets to high-performance thermoplastic cassettes—serve as the foundation for infection prevention and procedural efficiency.
As global surgical procedures increase in complexity, custom OEM/ODM tray design has transitioned from passive holders to active contributors to surgical outcomes. Advanced trays mitigate micro-motion damage during transport, optimize steam/sterilant penetration, and ensure complete ergonomic compliance for surgical teams.
Selecting appropriate materials is paramount when developing OEM surgical cassettes. Our engineering department specializes in evaluating thermal tolerance, mechanical impact resilience, chemical resistance, and biostability:
Trays are engineered for optimal fluid and thermodynamic dynamics. Perforated matrix patterns promote rapid moisture evacuation during vacuum drying phases while allowing uniform exposure to Ethylene Oxide (EO), Hydrogen Peroxide Gas Plasma, or Autoclave steam cycles in compliance with ISO 17665 and ISO 11135.
Through our rapid ODM framework, we transform client 3D models into functional physical prototypes within 14 business days. Utilizing high-precision CNC machining and custom injection molding, we guarantee dimensional tolerances down to ±0.02mm.
Trays are designed with double-hinged latching mechanisms, silicone edge protectors, stackable feet corners, and lightweight composite walls to reduce fatigue among sterile processing technicians and prevent glove tears.
Tailored tray system architectures engineered for specific clinical environments, regional hospital protocols, and specialized medical fields.
Orthopedic procedures require complex multi-tiered tray systems containing dozens of drills, reamers, plates, and screws. Our customized OEM trays feature removable color-coded caddies, printed size graphics, and lockable silicone retention brackets that prevent component mixing during transportation and washing.
Flexible and rigid endoscopes feature delicate optical fiber systems easily damaged by standard cleaning routines. Our specialized scope cassettes incorporate soft silicone spring-loaded nests, dedicated flushing ports, and integrated protective covers engineered for high-level disinfection (HLD) and low-temperature gas plasma sterilization.
For high-turnover dental clinics and oral surgery suites, our compact modular cassettes streamline instrument organization from chairside treatment to ultrasonic bath cleaning and autoclaving. Quick-release latches ensure swift sterilization cycles and organized storage.
Pioneering smart medical packaging through digital tracking, sustainable material innovation, and automated manufacturing.
Embedding heat-resistant UWB RFID chips directly into surgical tray handles. This allows real-time automated tracking of instrument tray locations across CSSD cleaning, autoclaving, operating rooms, and storage inventories, reducing manual counting errors to absolute zero.
Transitioning from traditional fossil-derived plastics to bio-based, fully recyclable PPSU composites. These eco-friendly materials maintain identical structural strength and heat resistance while reducing carbon footprint across manufacturing cycles by over 40%.
Leveraging generative AI algorithms to auto-design internal tray geometry based on 3D scans of custom instrument sets. This optimizes space utilization by 30%, minimizes overall tray weight, and improves steam flow efficiency.
Why international medical device brands and hospital networks choose our integrated manufacturing hub for long-term strategic partnerships.
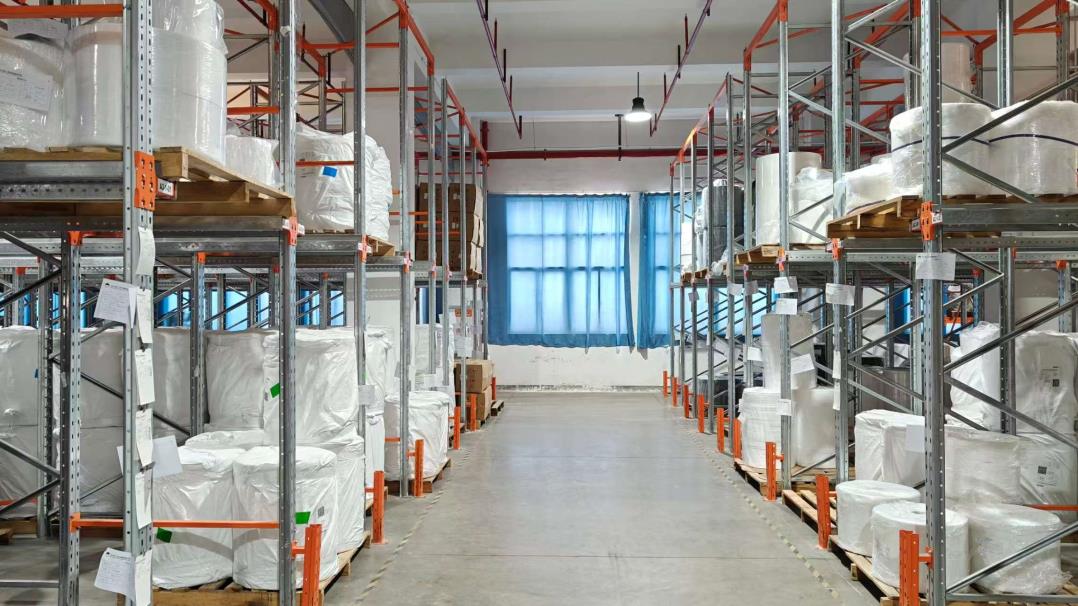
By housing raw material synthesis, precision metal stamping, plastic injection molding, cleanroom assembly, and packaging under one corporate umbrella, we eliminate third-party supply delays. Our 100,000 m² footprint and centralized supply chain node in China ensure stable procurement, buffer inventories of high-grade raw polymers, and immune response to global logistic fluctuations.
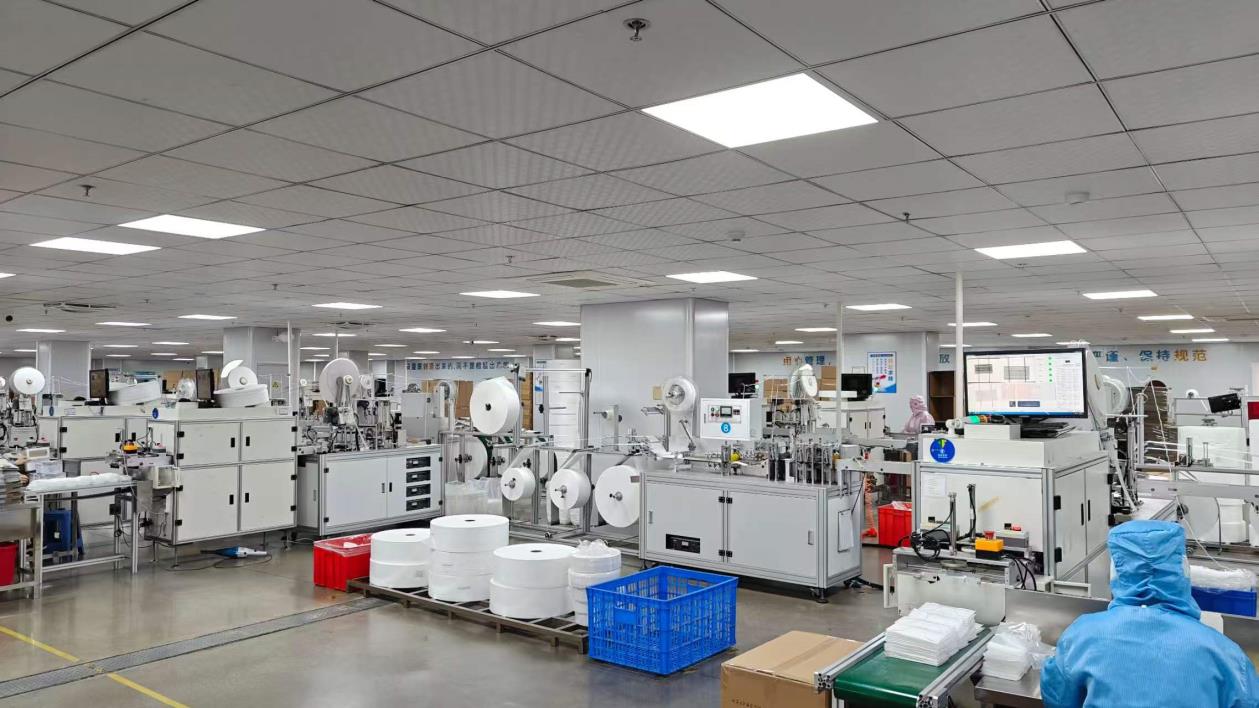
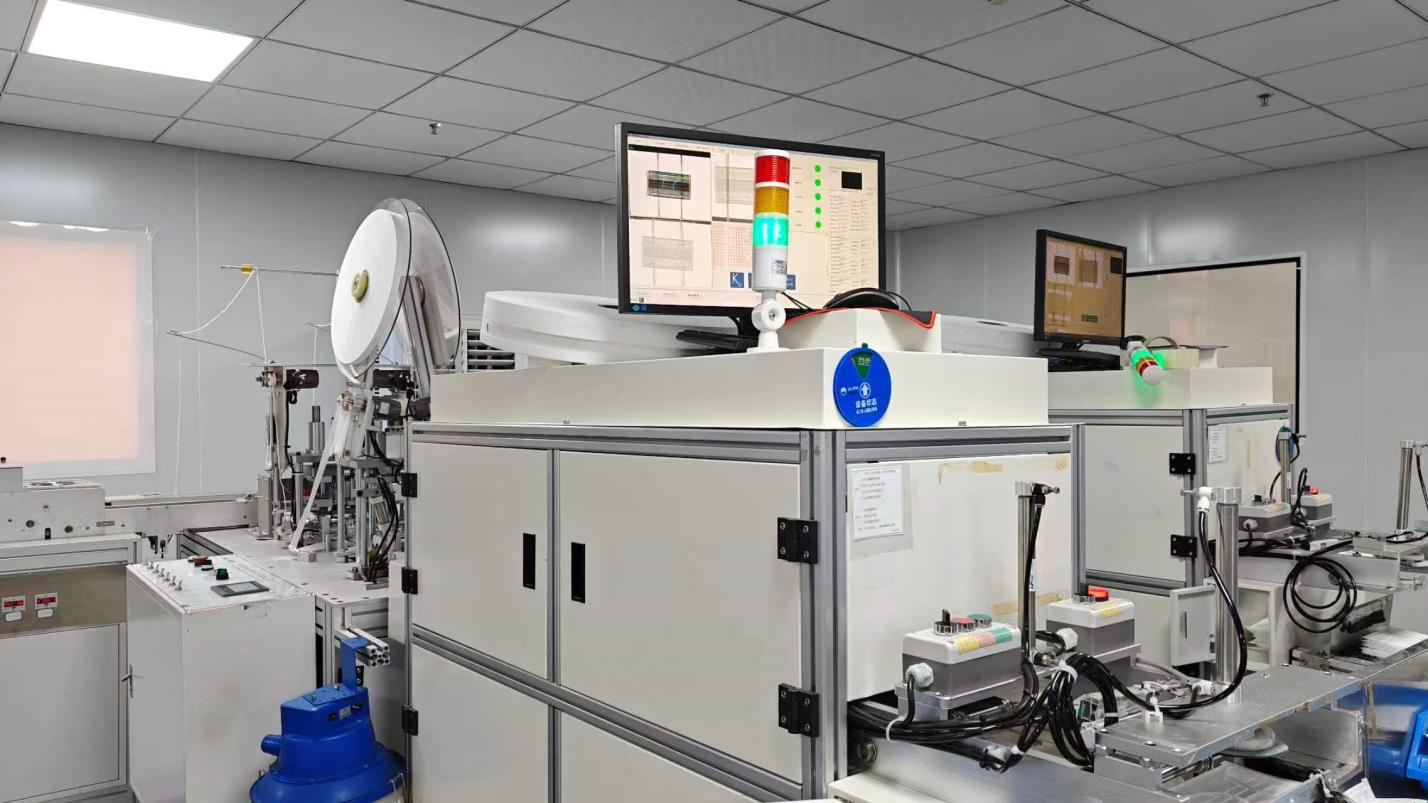
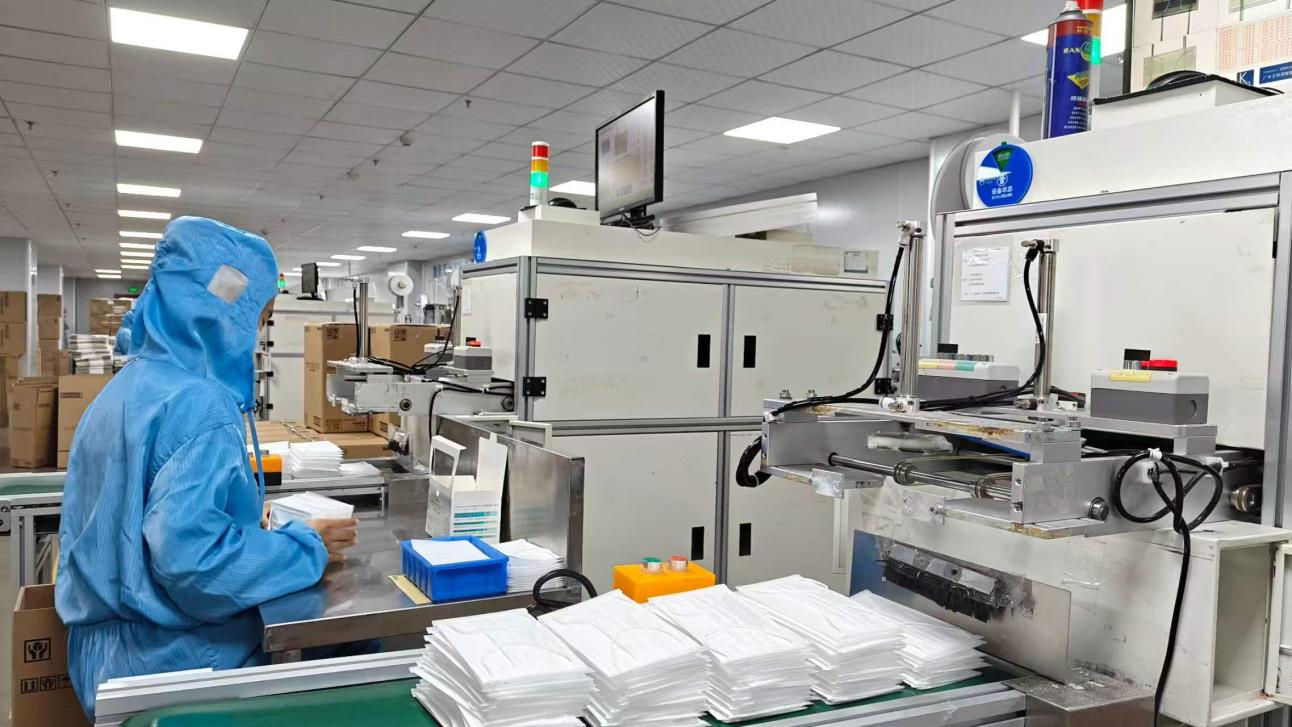
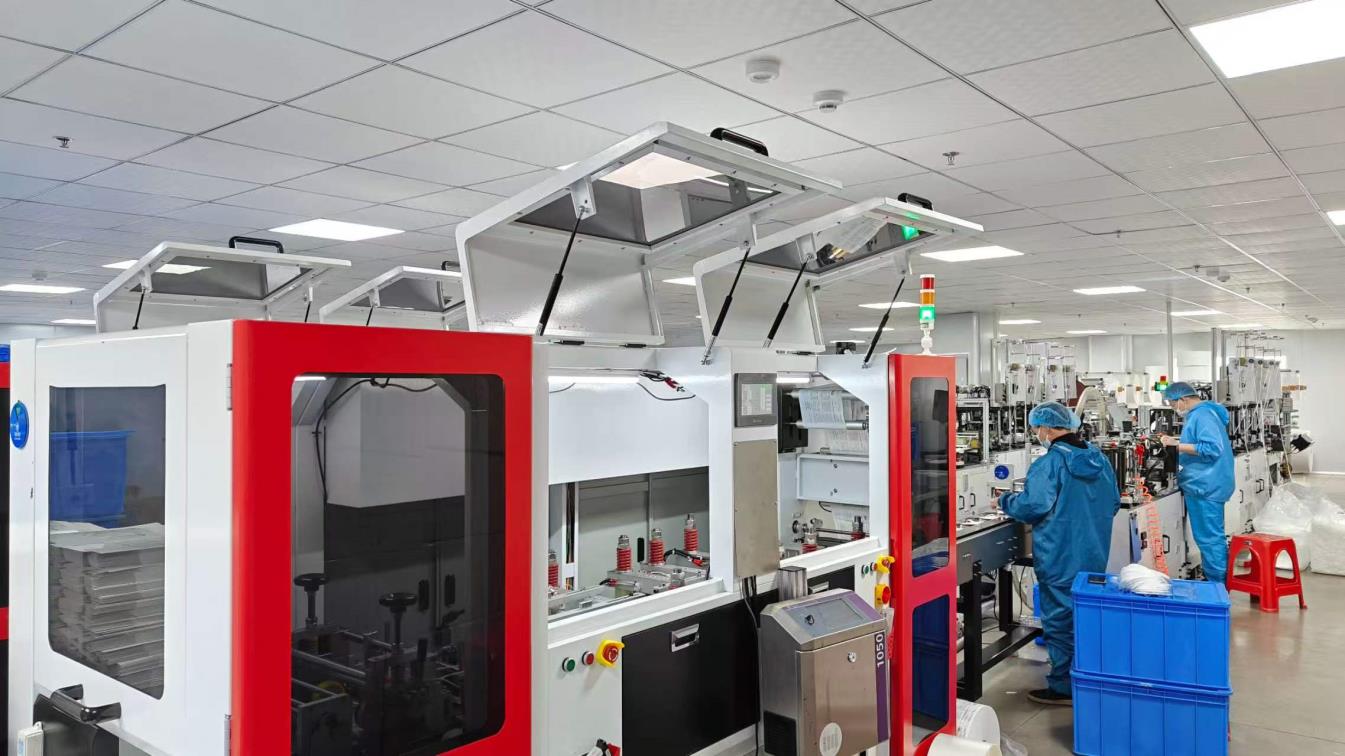
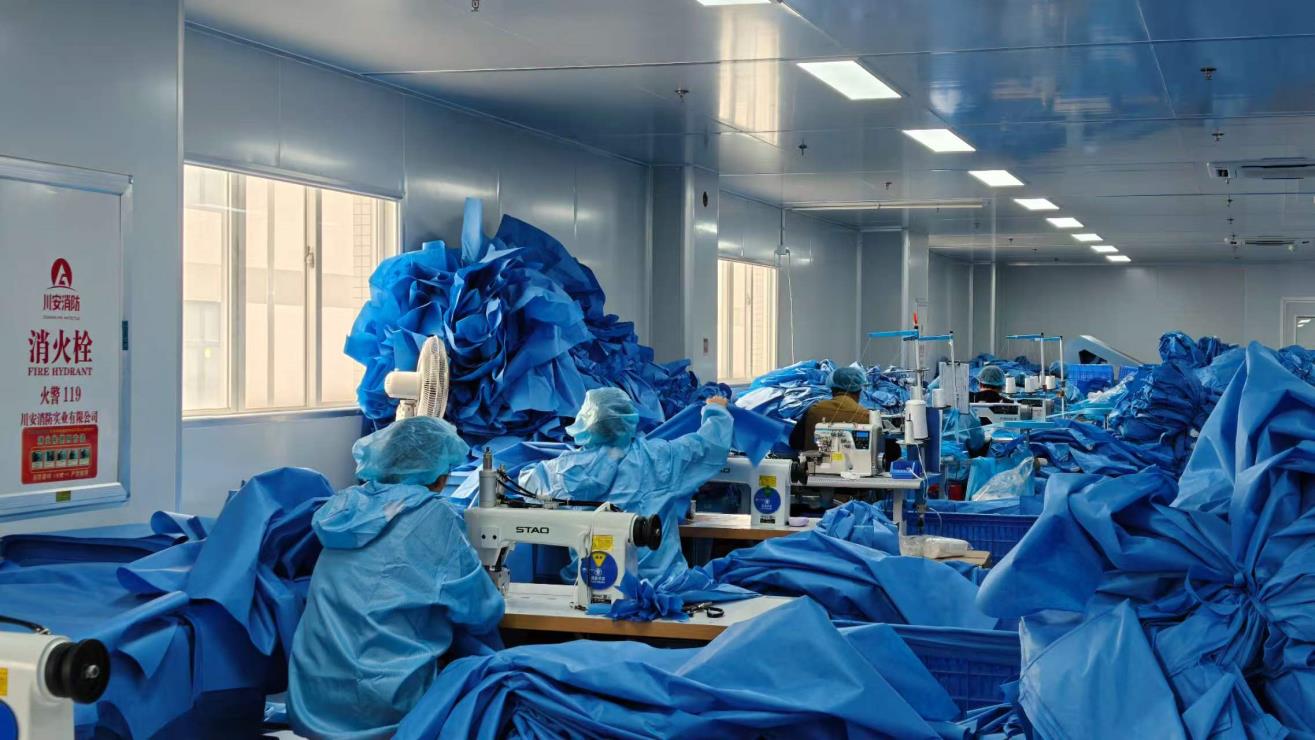
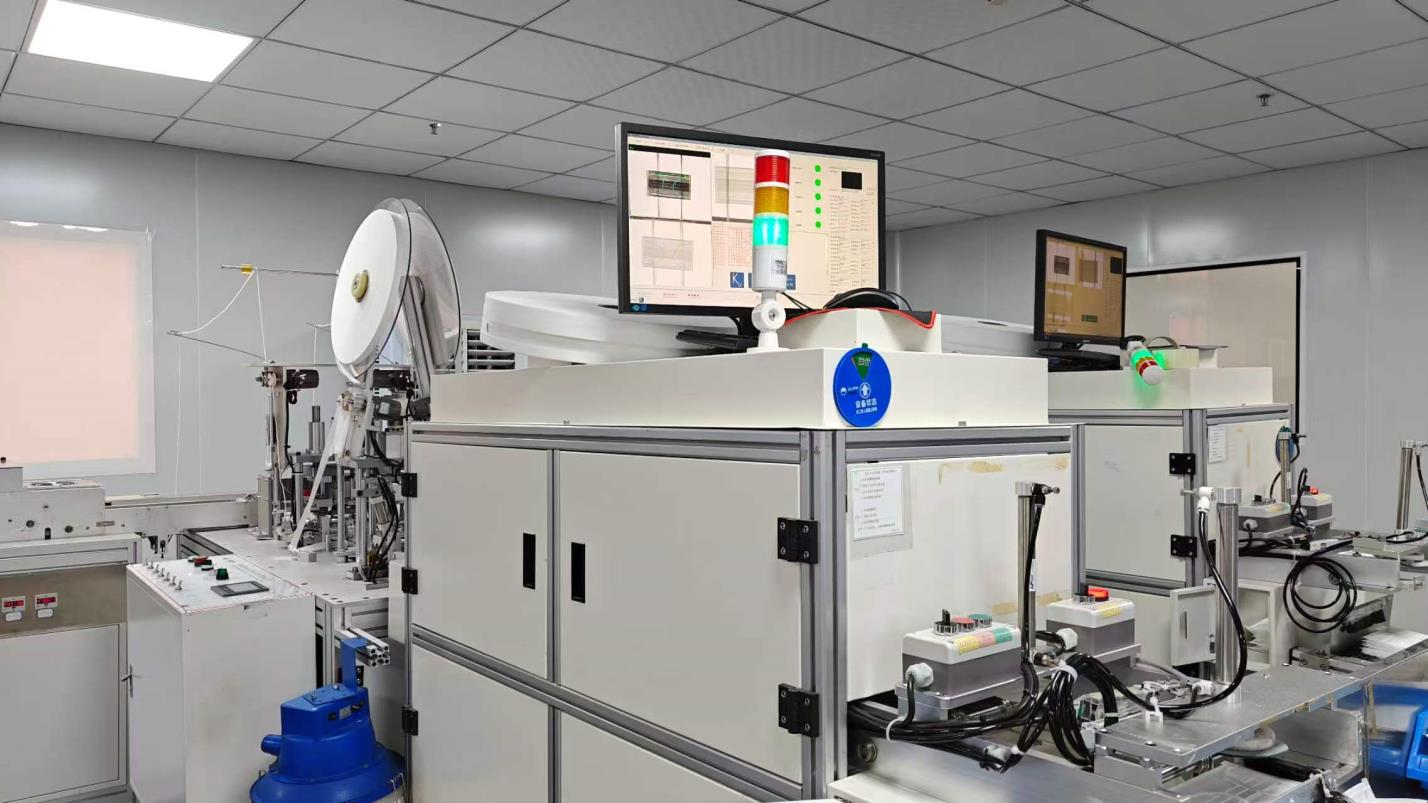
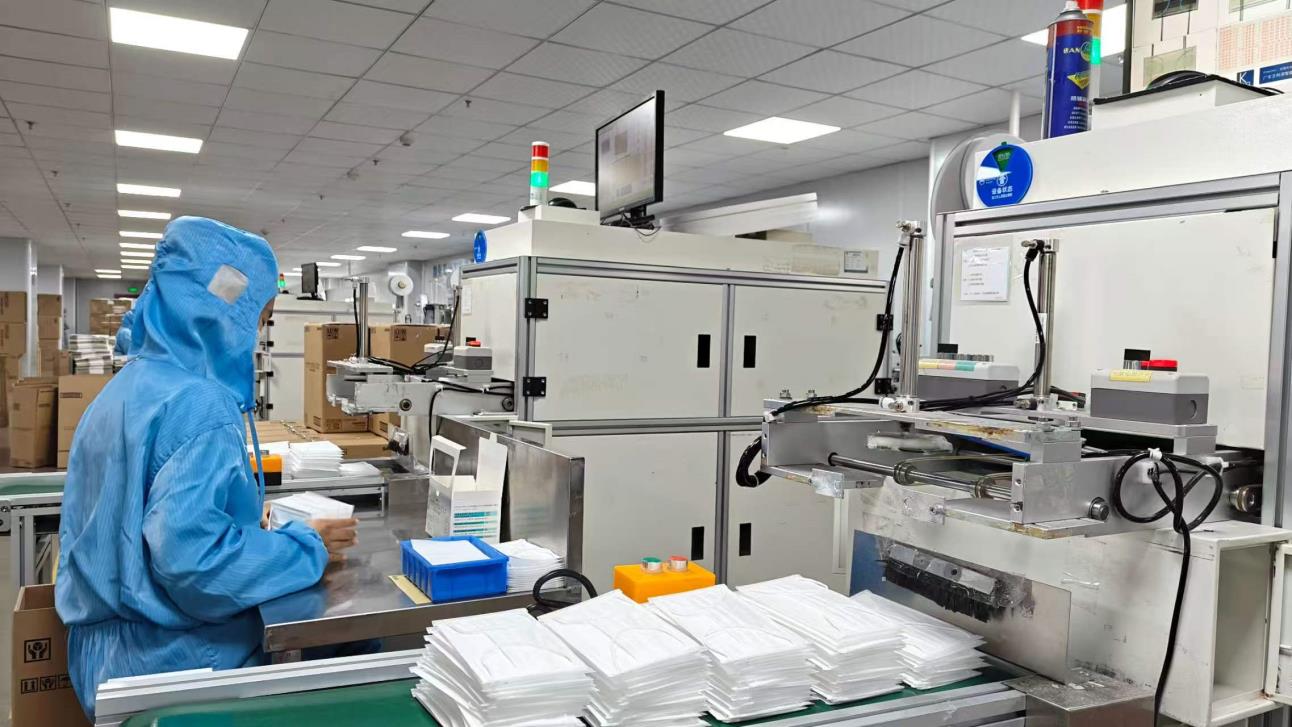
With automated production lines, 500+ skilled personnel, and 6,000 m² of Class 8 cleanrooms, our facility yields unmatched economies of scale. Overseas partners benefit from a 30-45% reduction in total landed manufacturing costs without sacrificing micro-tolerances or regulatory integrity.
Our facility operates comprehensive automated production equipment along with a state-of-the-art Quality Control (QC) laboratory to guarantee full regulatory compliance for every shipment.
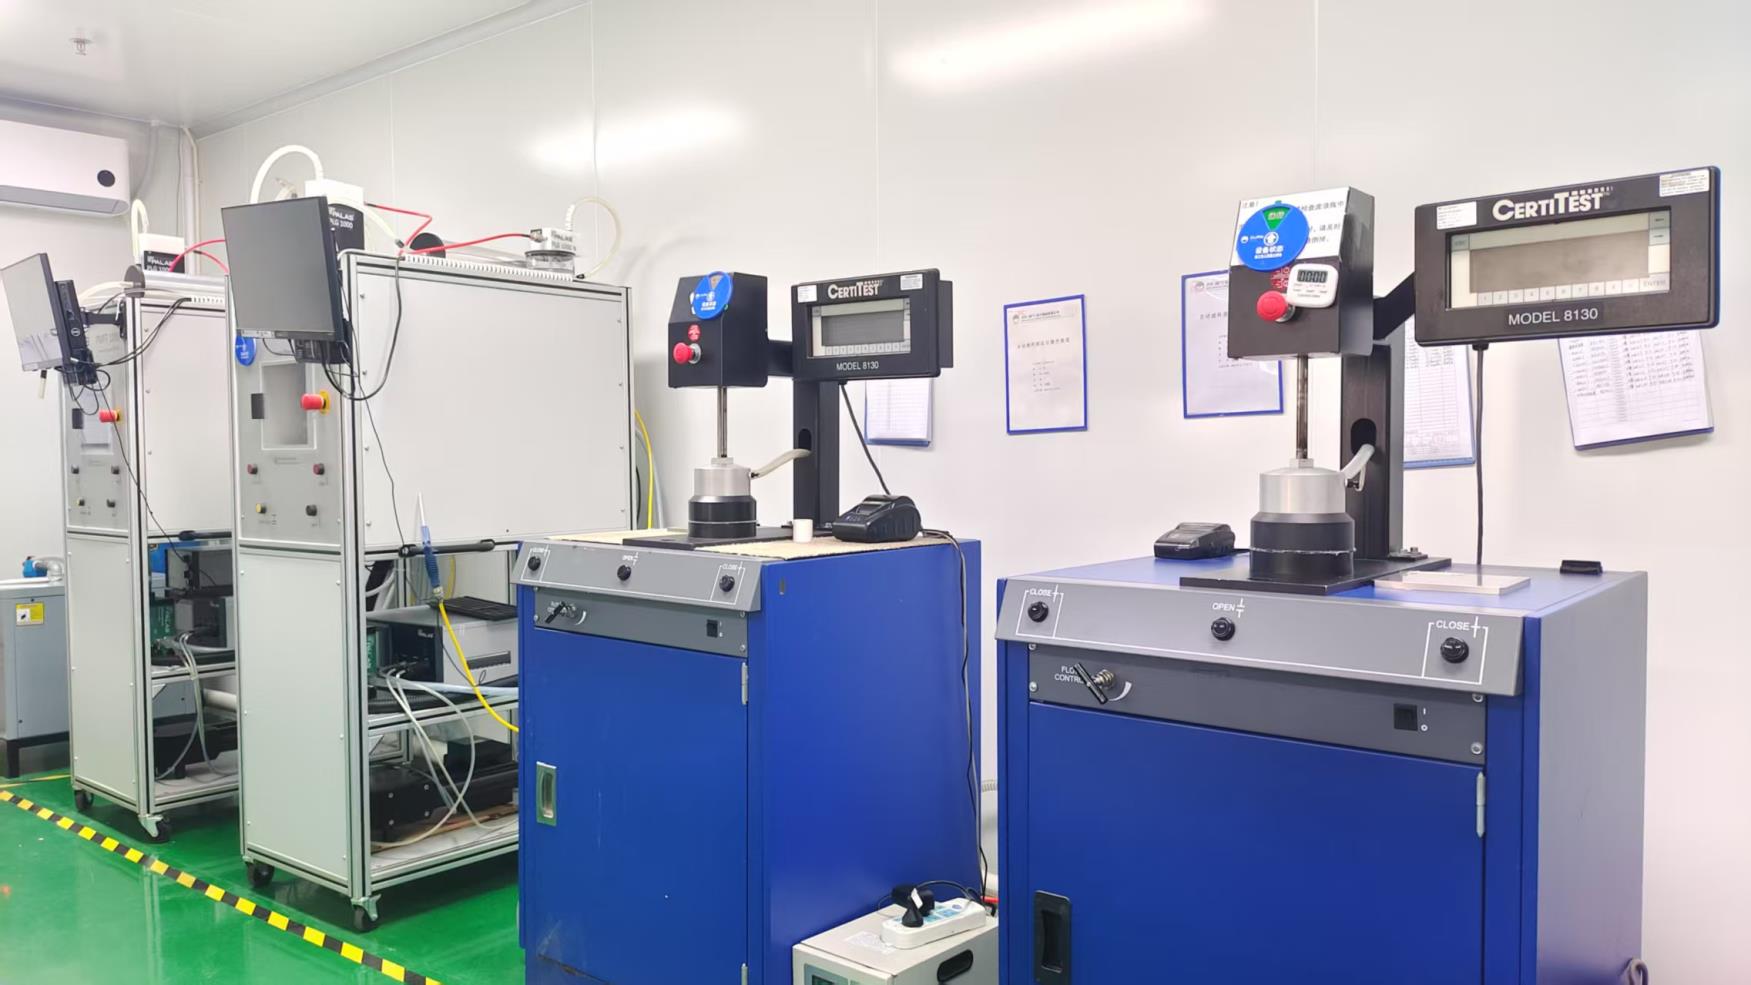
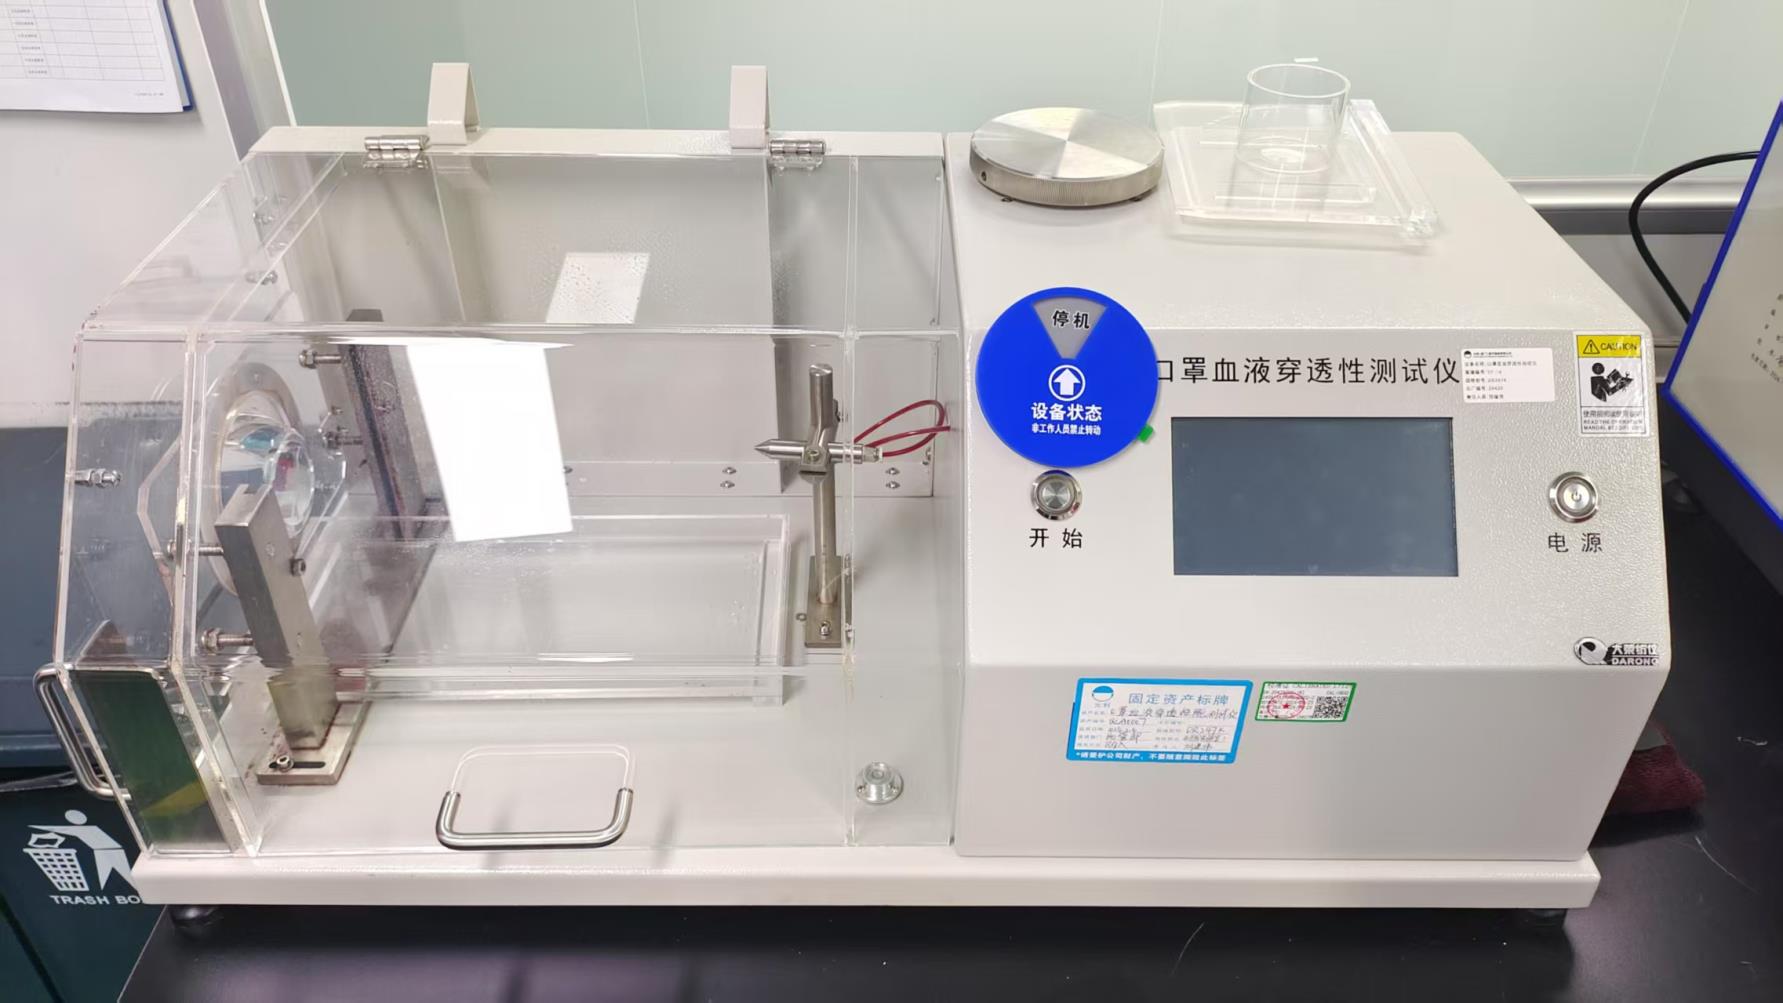
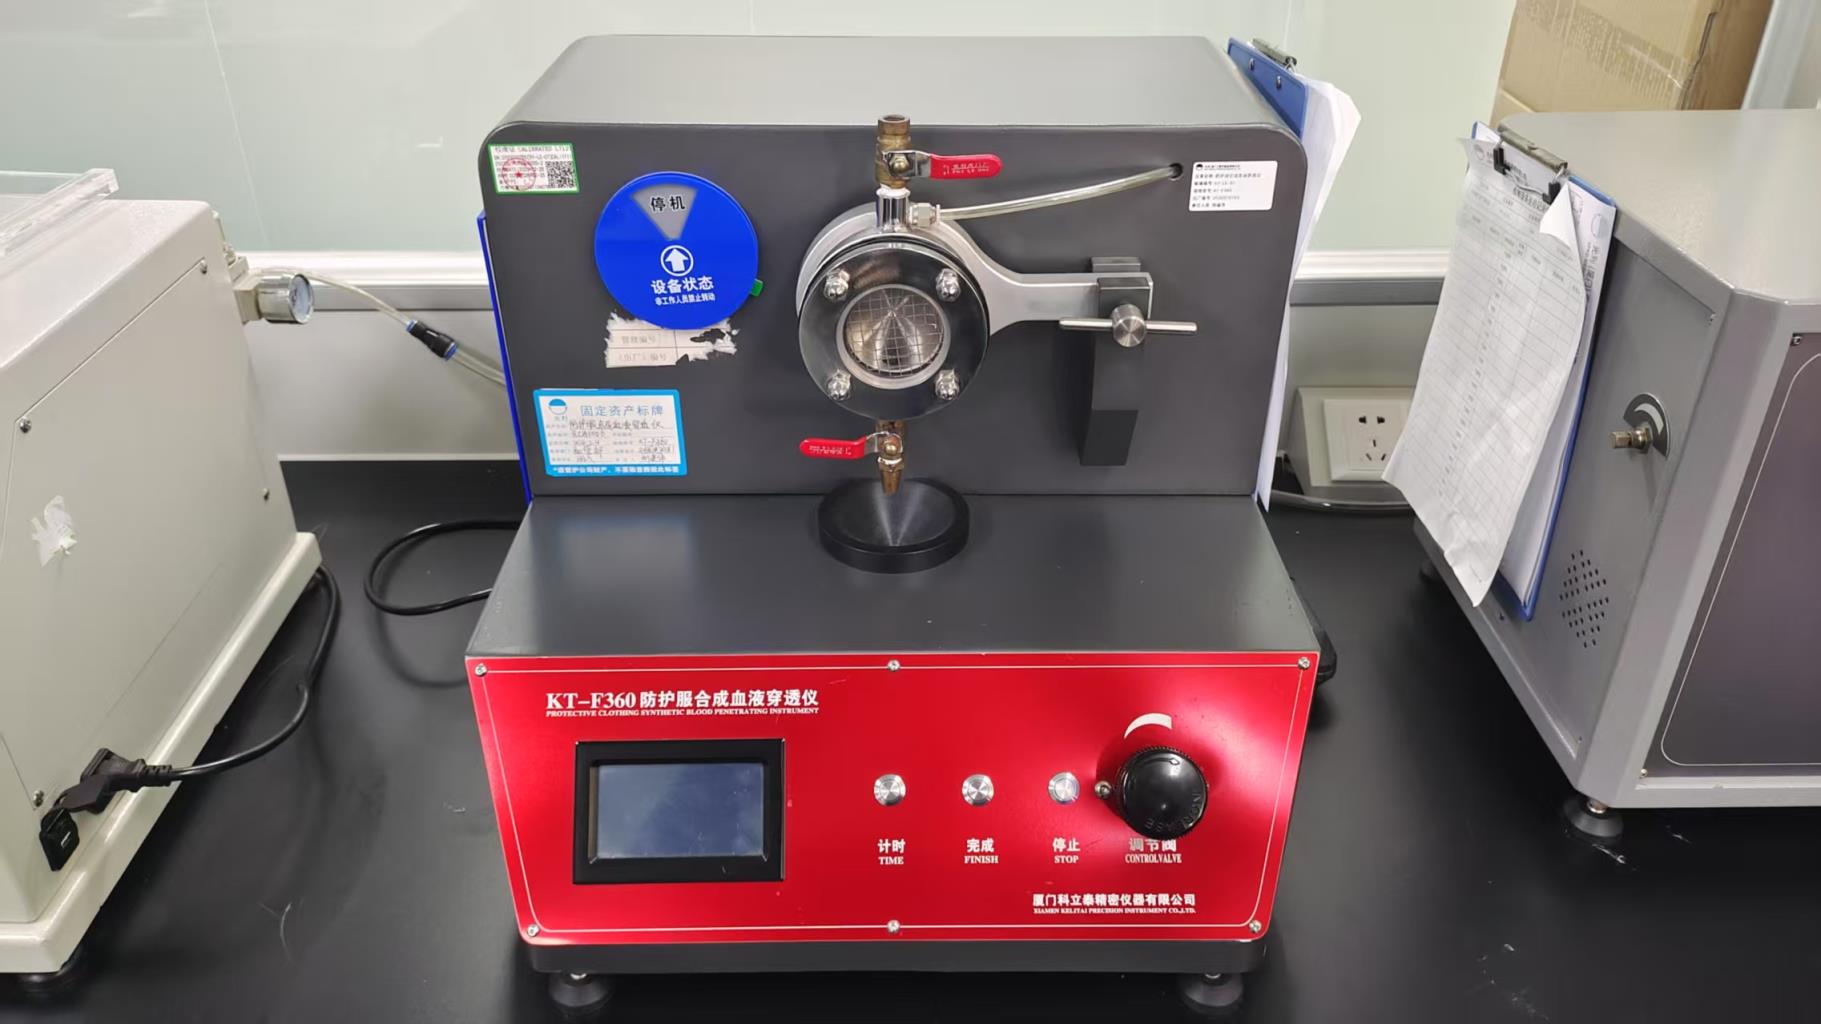
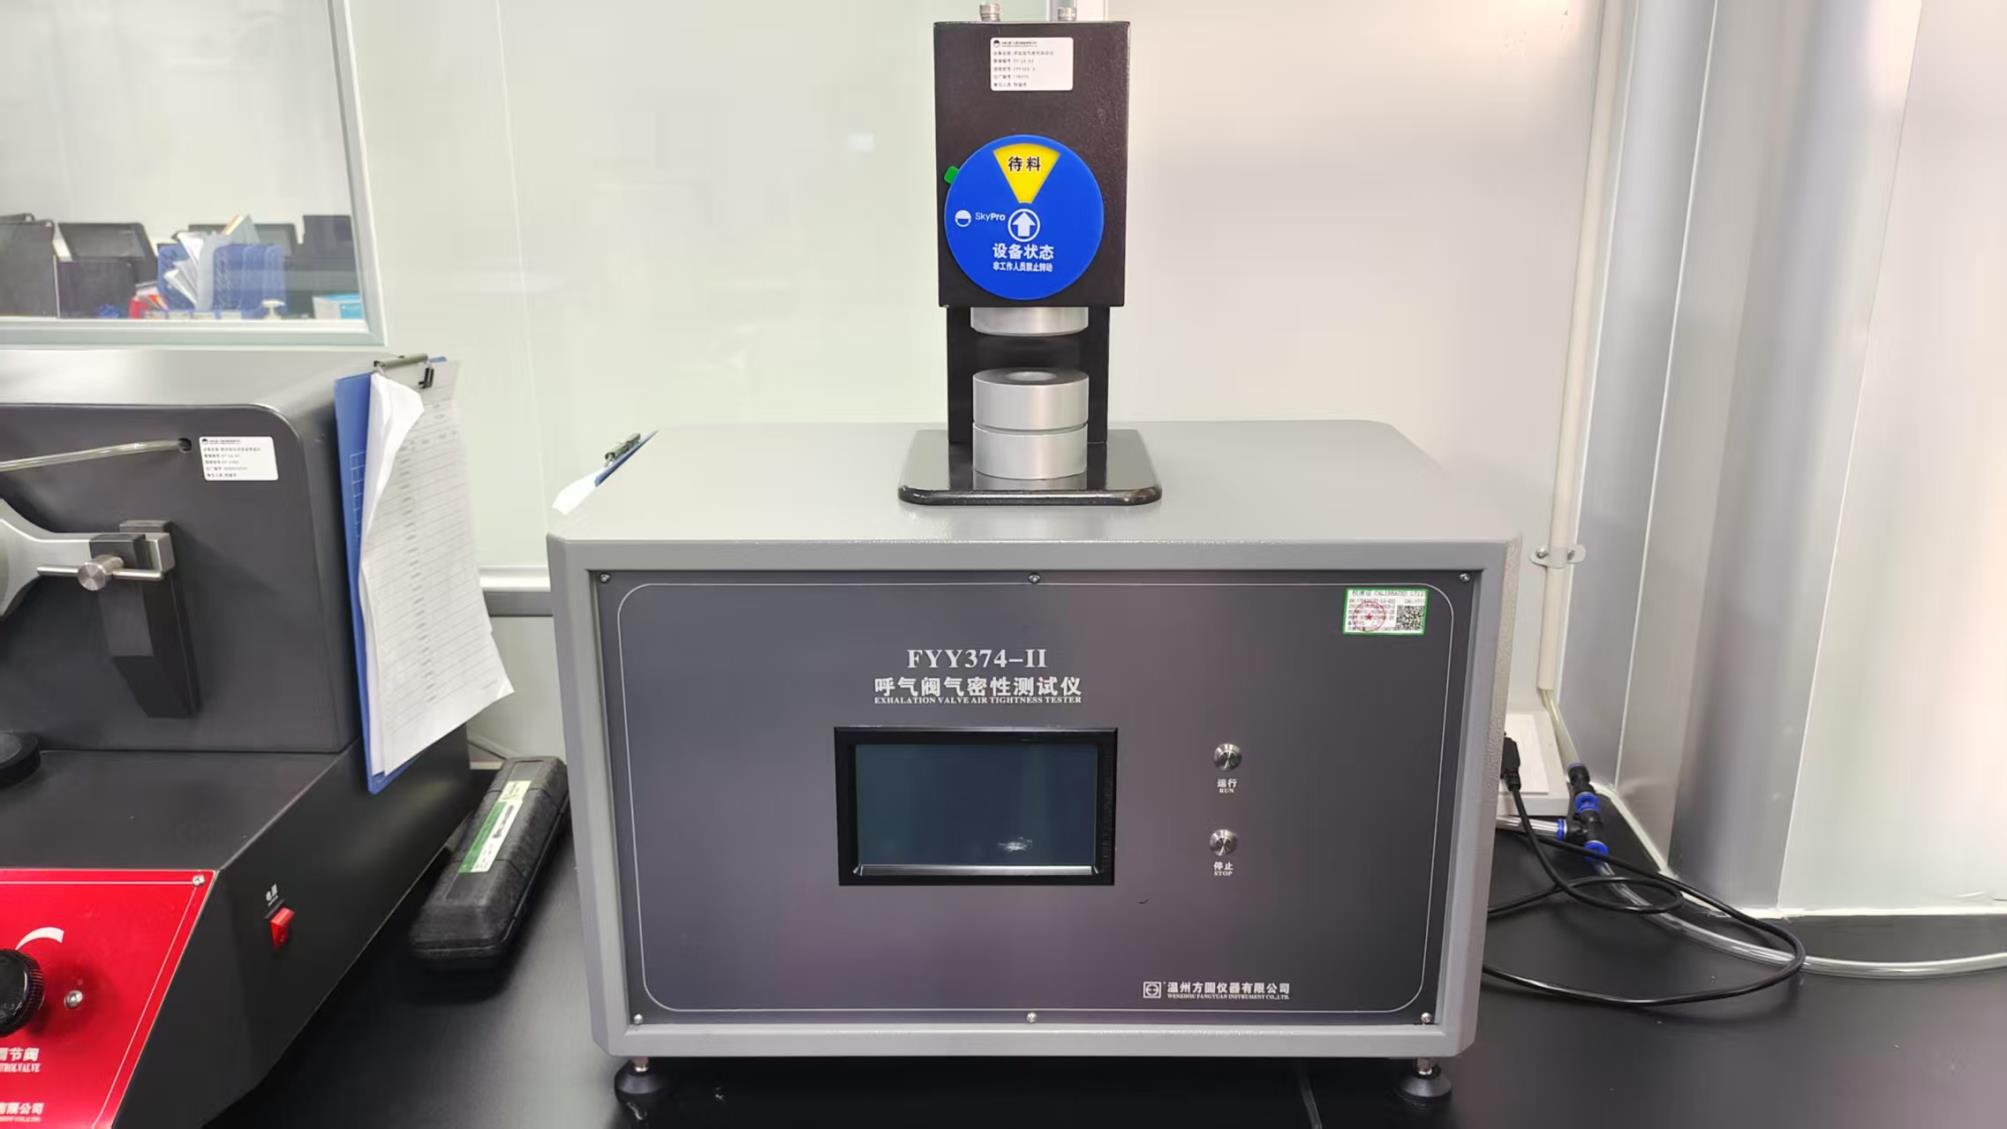
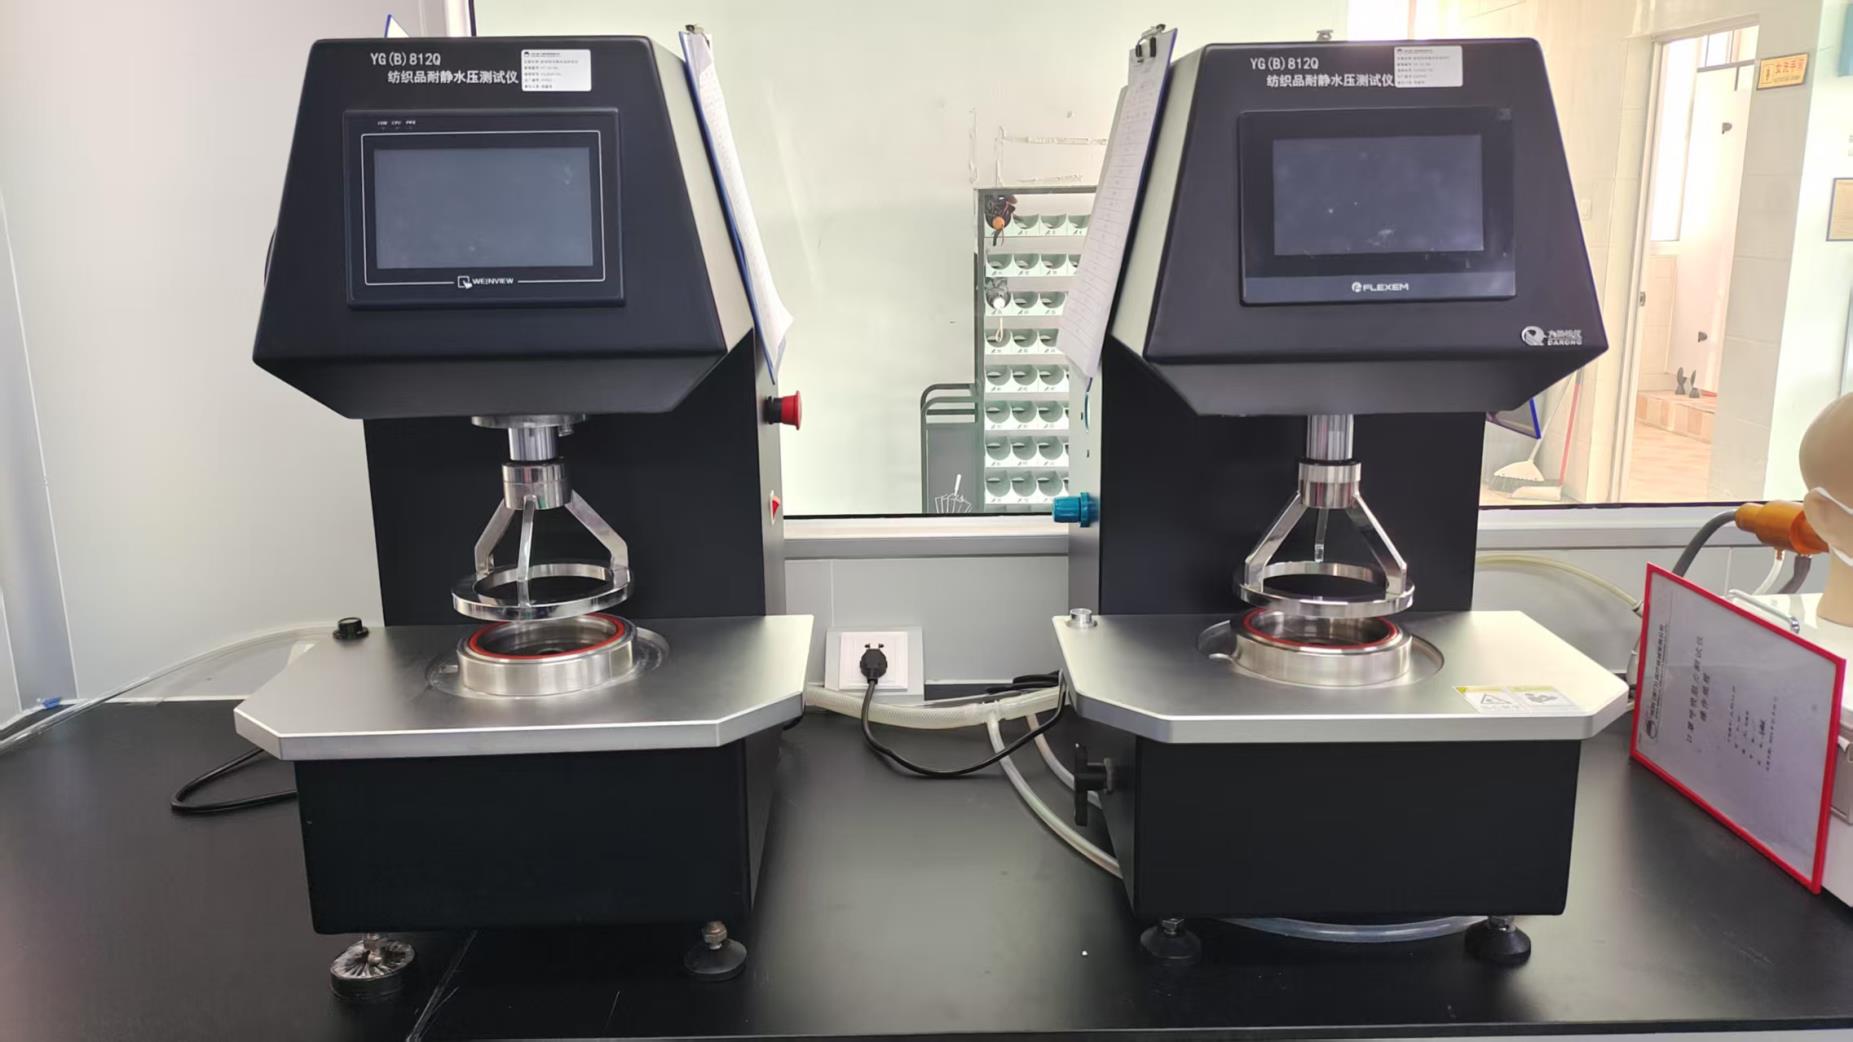
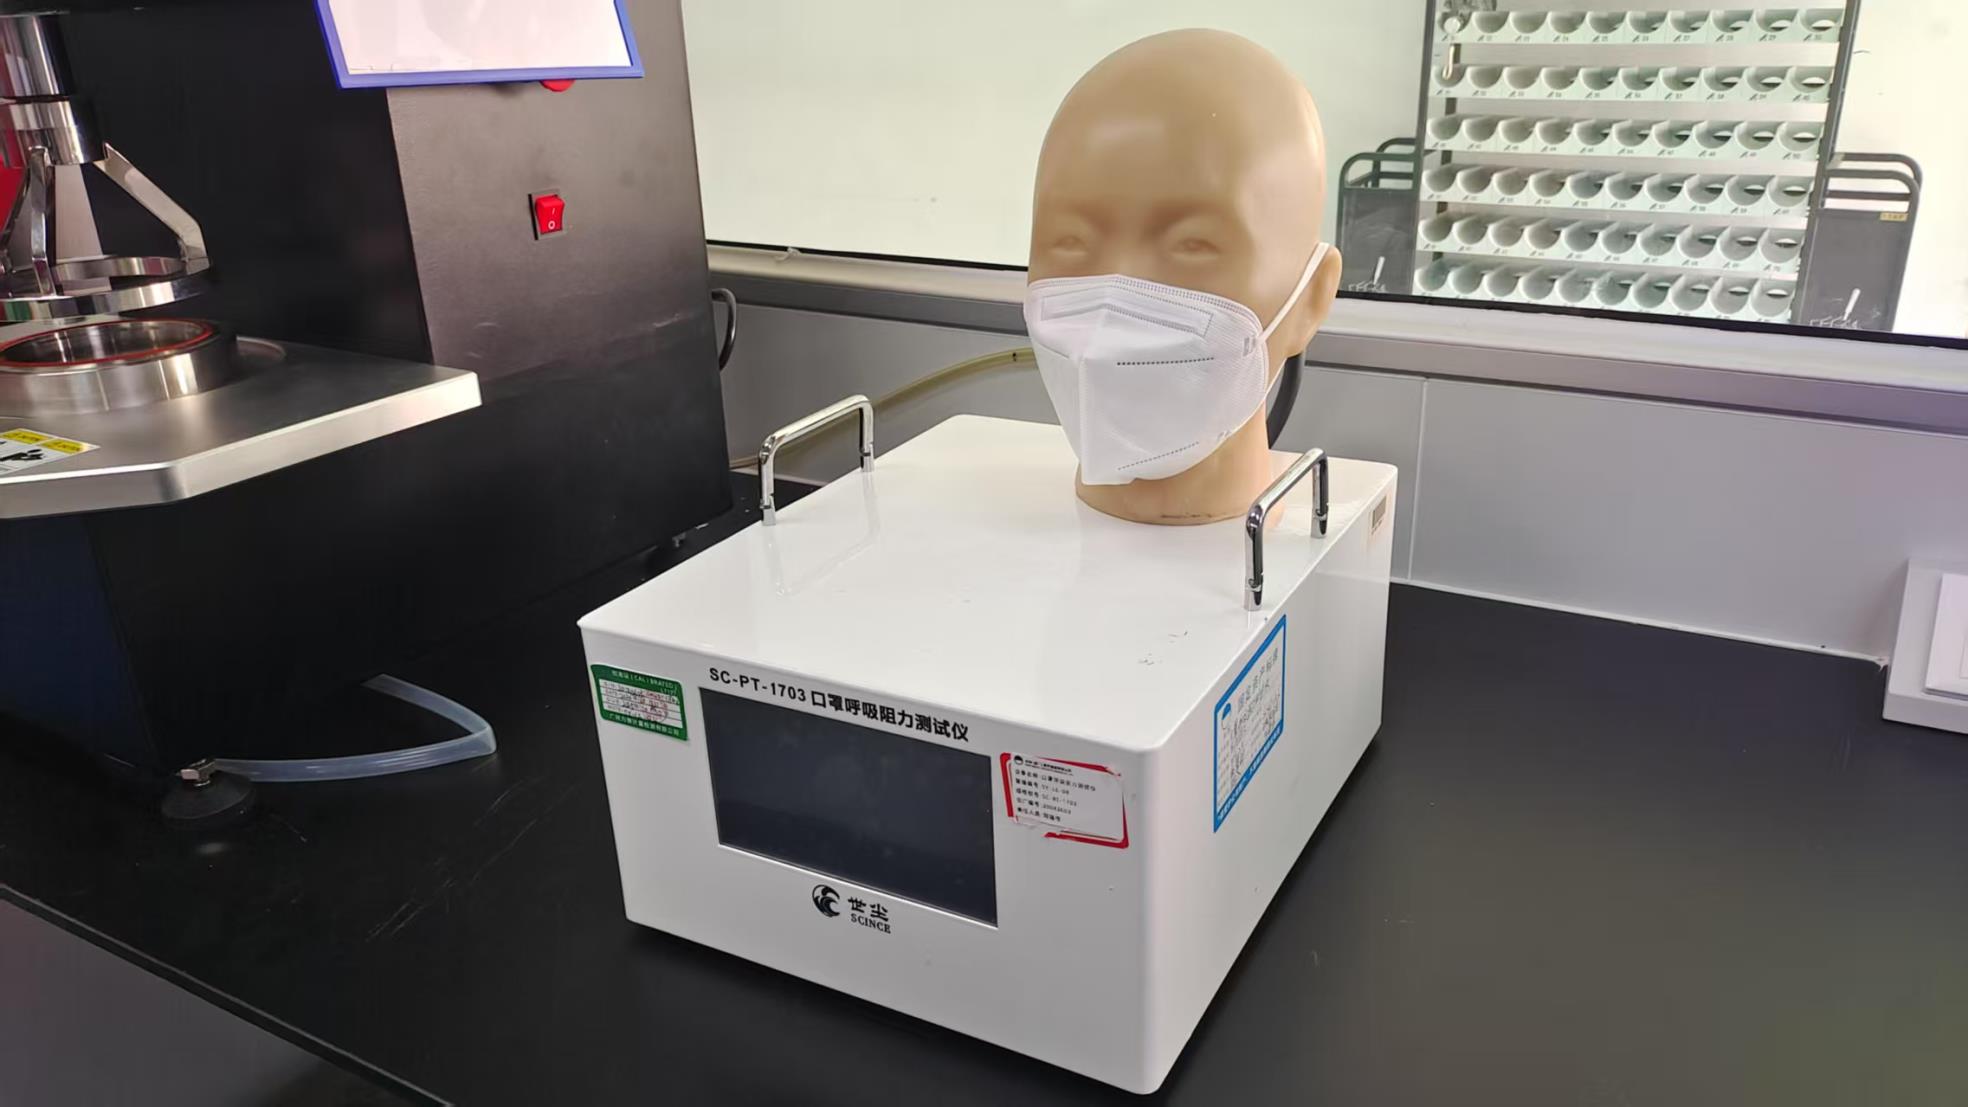
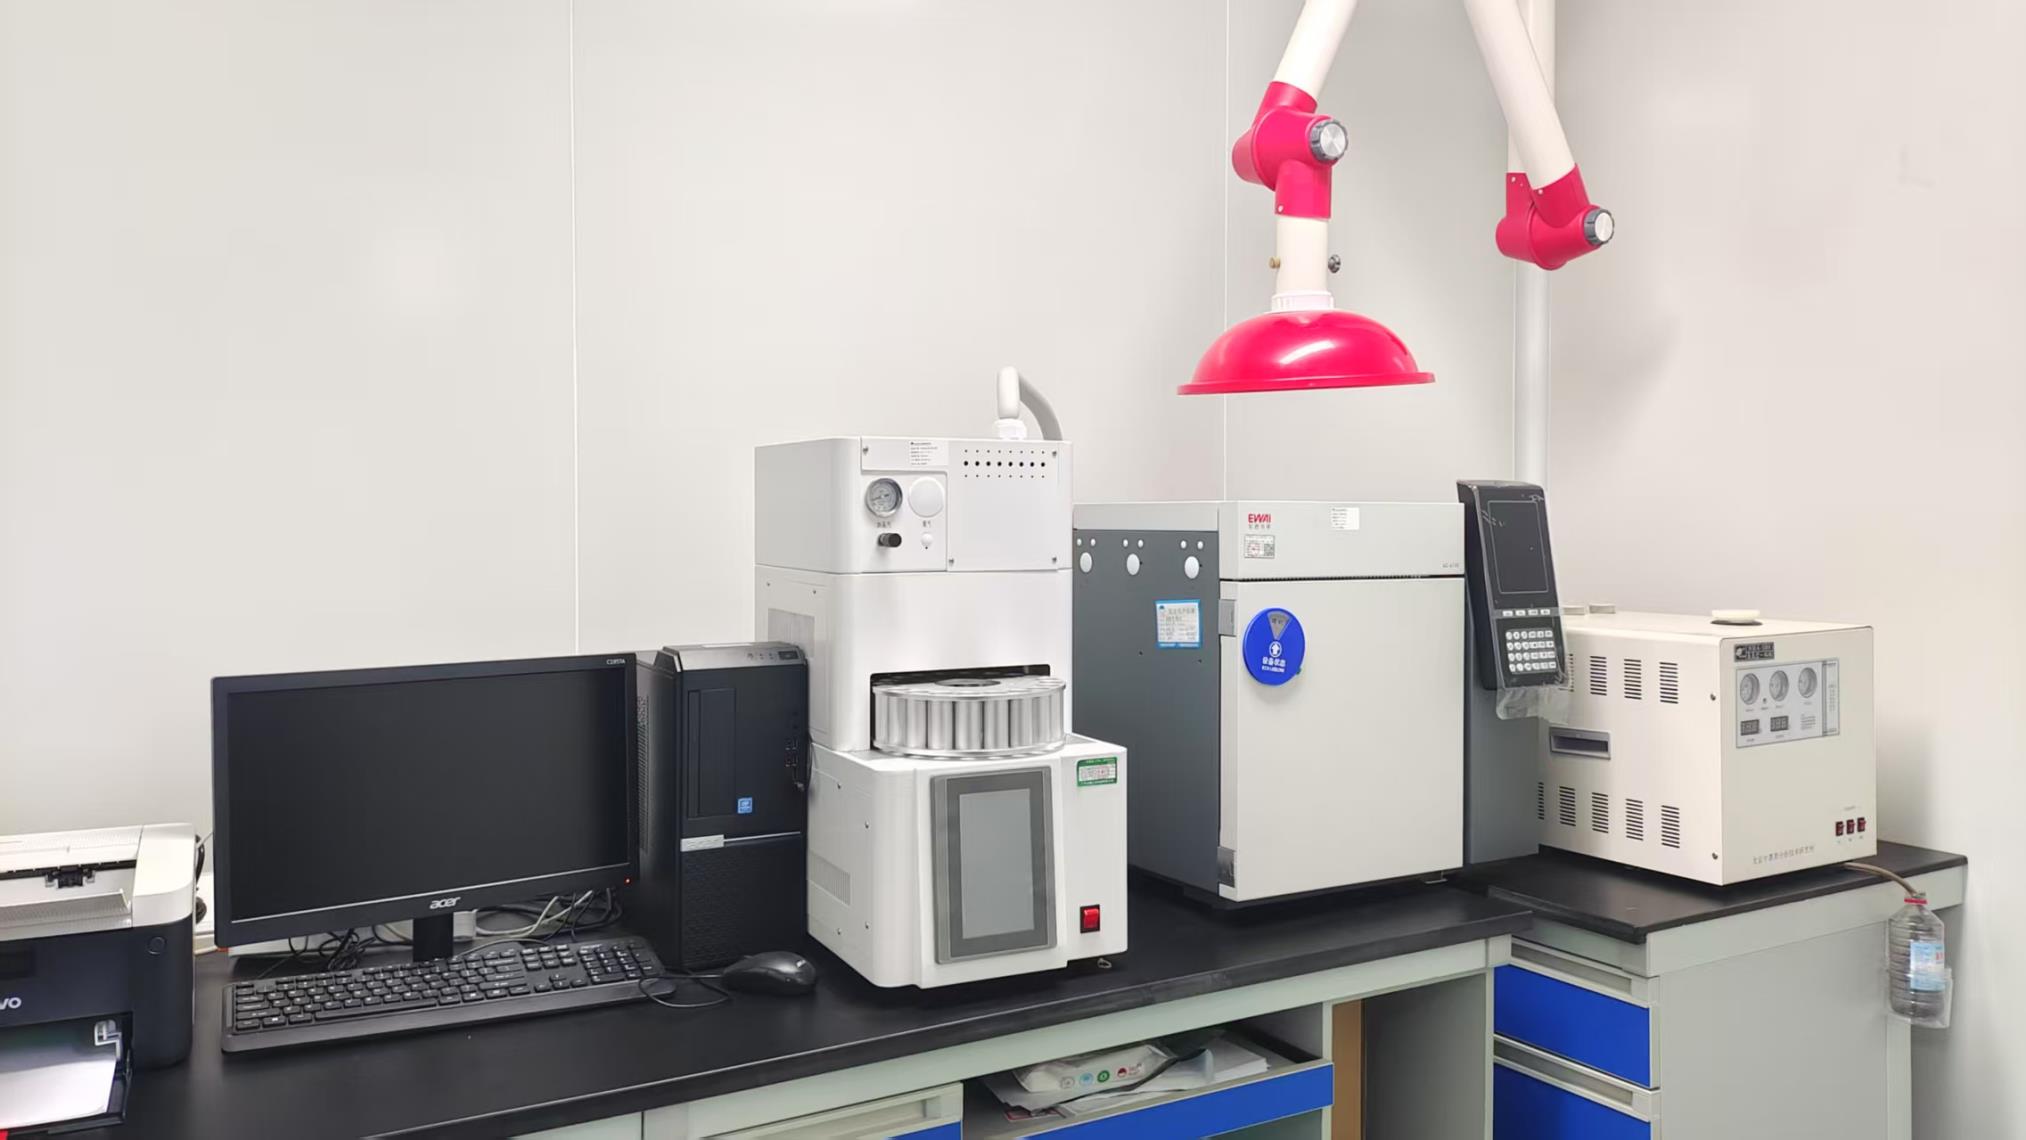
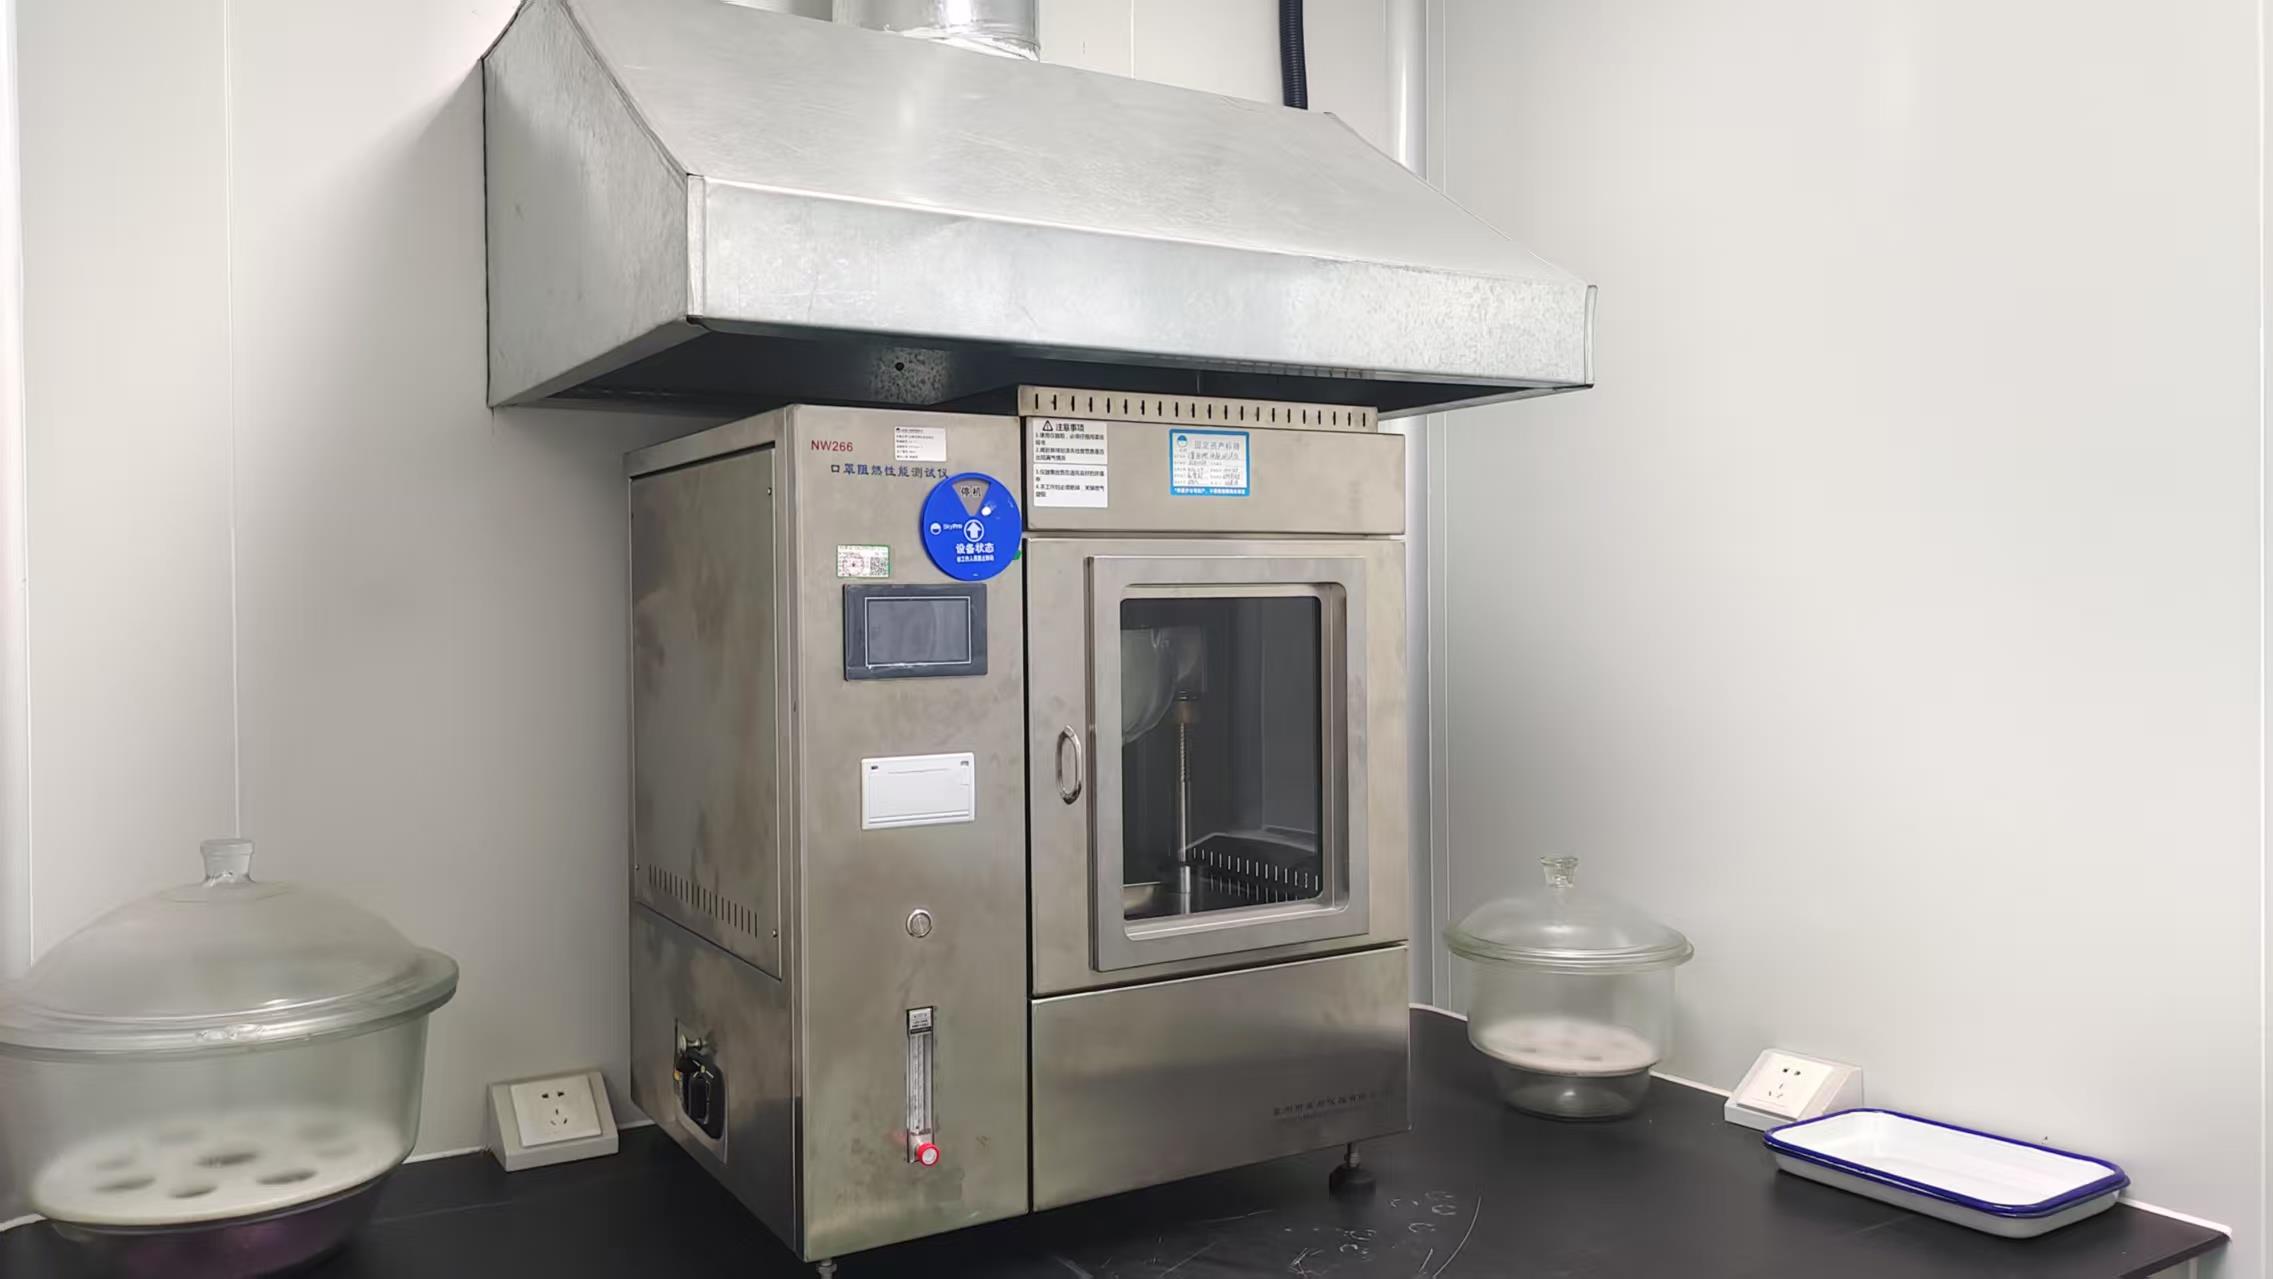
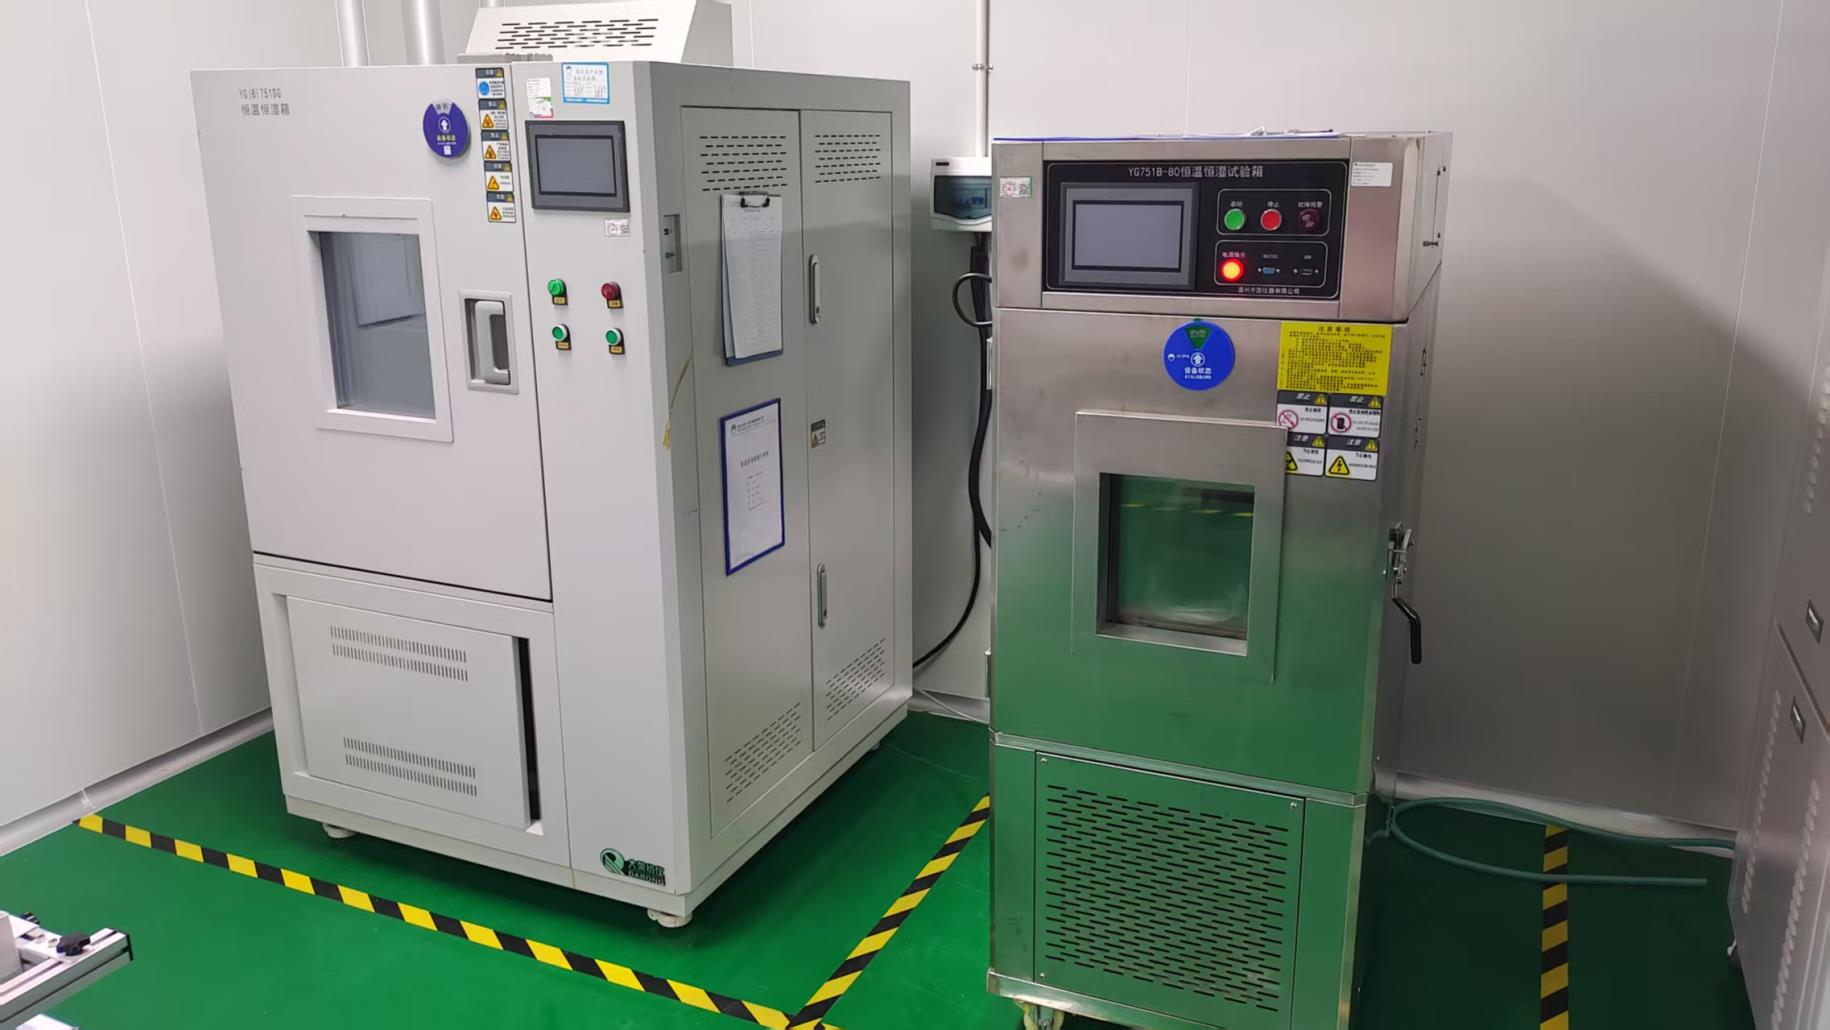
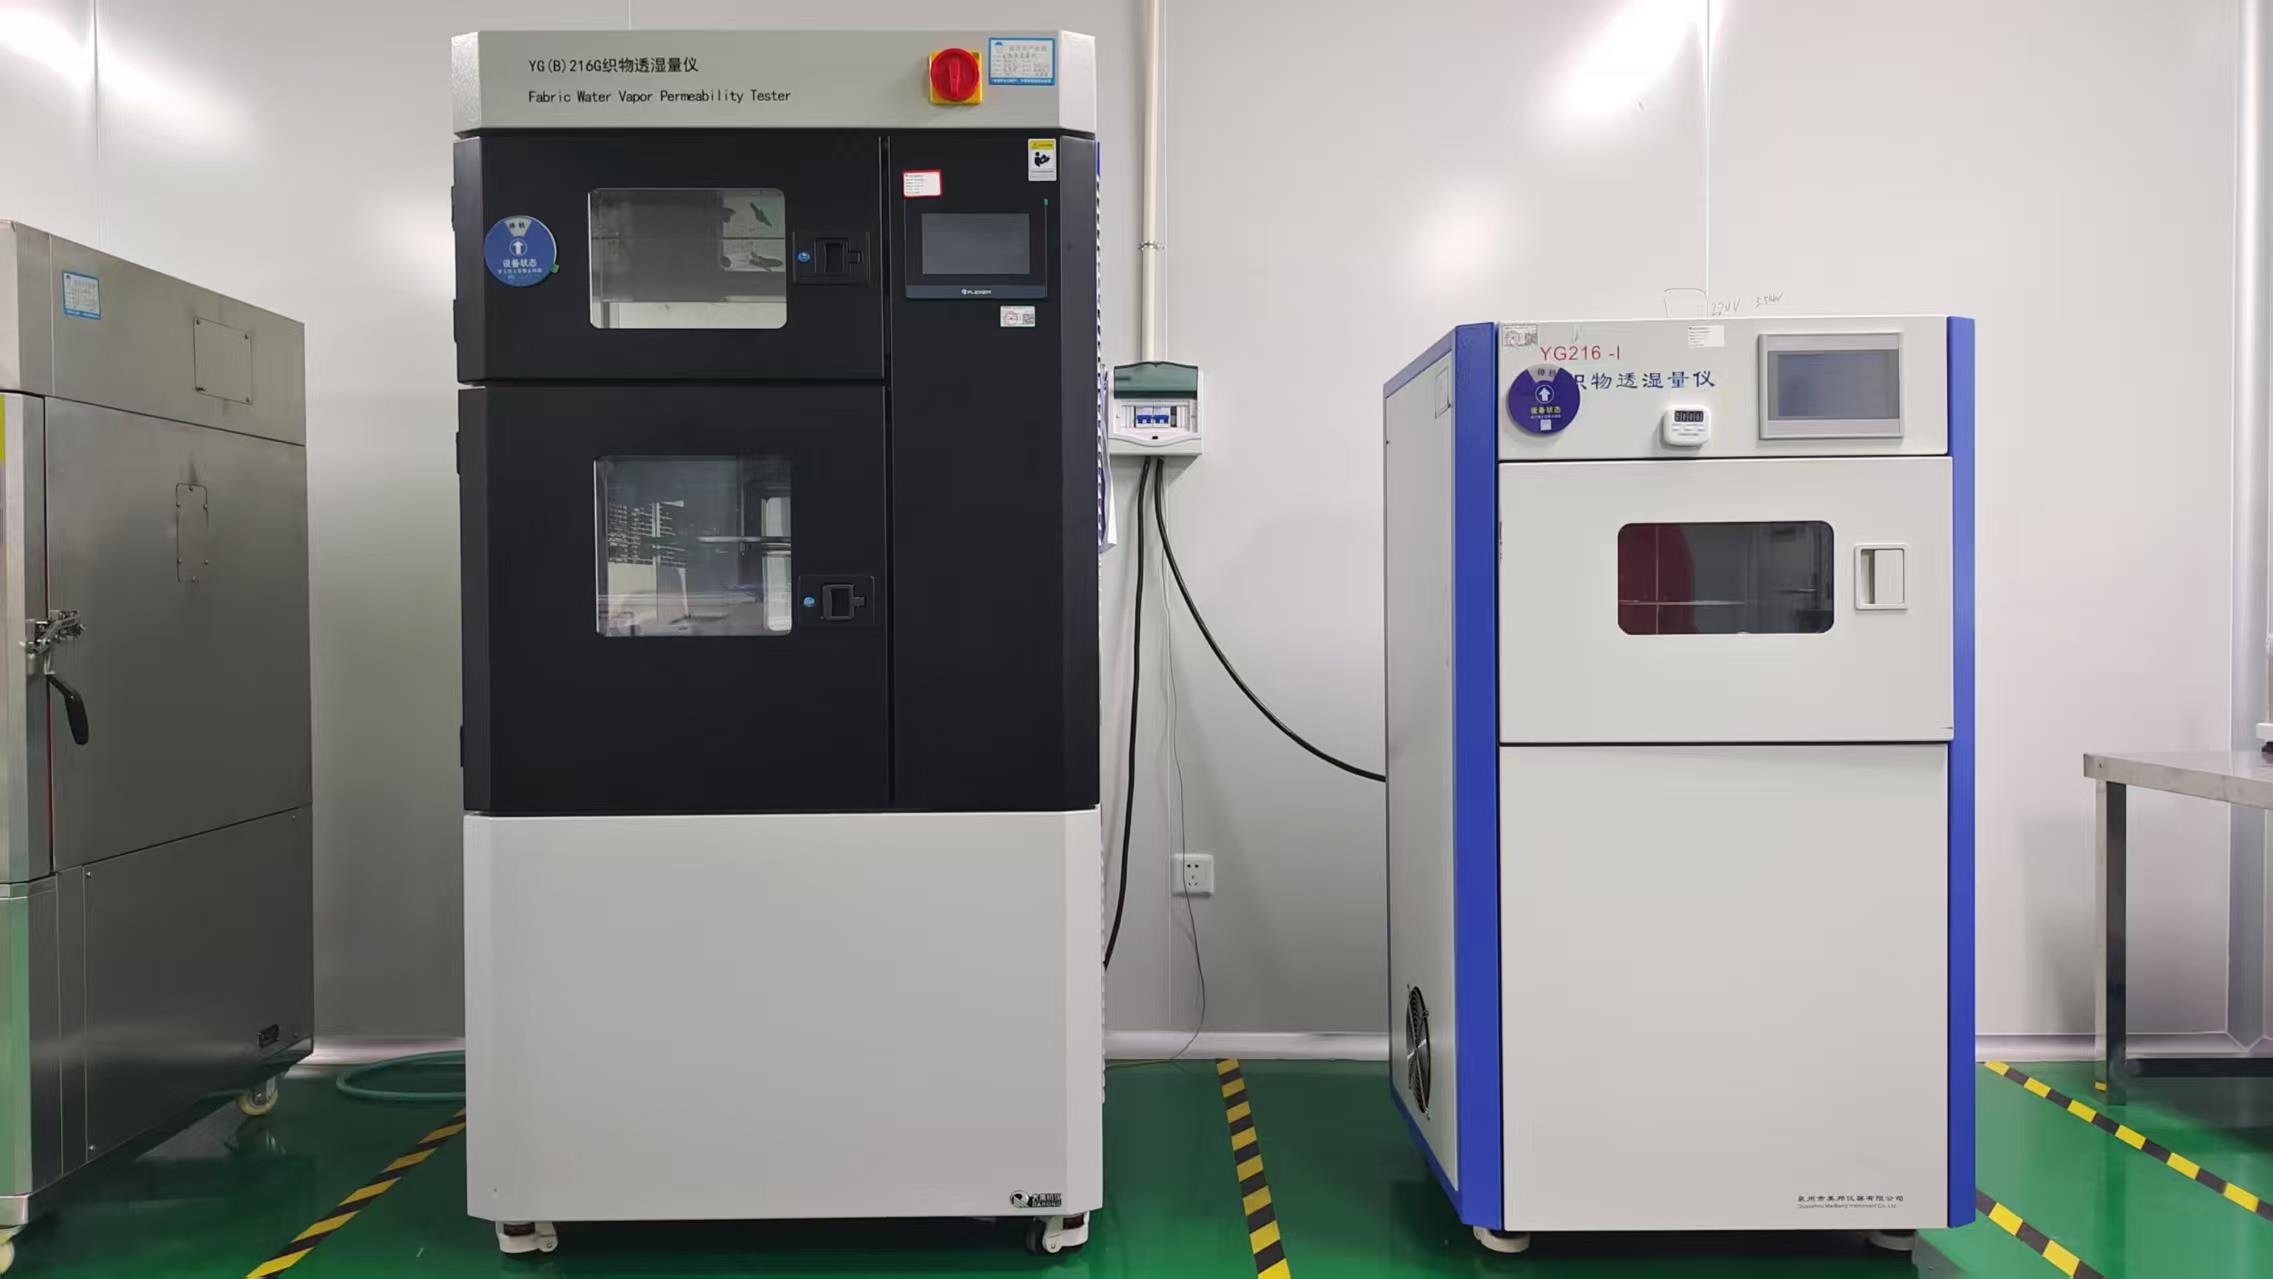
Navigating complex international medical device regulations (MDR/FDA) through comprehensive technical documentation, batch traceability, and validation protocols.
Our engineering documentation packages support complete Technical File preparation for European Class I and Class IIa medical devices. We provide full material bio-compatibility evaluations according to ISO 10993 series.
We maintain Device Master Files (DMF) for international clients, streamlining submittals for U.S. FDA 510(k) clearances. All tray designs undergo rigorous drop testing, transport simulation, and sterile barrier integrity testing (ASTM F1929 / ASTM F88).
Every product unit, box, and pallet supports localized Unique Device Identification (UDI) barcoding, GS1 standards, custom artwork, multilingual instructions for use (IFU), and brand-specific private labeling.
Answers to common commercial, engineering, and regulatory questions regarding OEM/ODM surgical instrument trays and protective healthcare products.
Discover our comprehensive range of specialized medical device components, diagnostic monitors, endoscopic tools, and cleanroom apparel.